


What Is a High Flux Longitudinal Fin Tube?
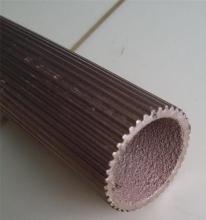
A high flux longitudinal fin tube is an extended-surface heat exchanger tube with fins running parallel to the tube axis, engineered for high heat flux density—the amount of heat transferred per unit area per unit time. In this context, "high flux" describes the tubes thermal duty per unit area, not a brand or proprietary grade. When heat flux reaches typical industrial reference levels of 30 to 100 kW/m² based on bare tube outer surface (typical range—final values must be confirmed by the project engineer and manufacturer data), a bare tube cannot transfer enough heat within the available temperature difference. Longitudinal fins solve this by enlarging the heat transfer area while keeping gas-side pressure drop relatively low.
Three features separate a high flux longitudinal fin tube from ordinary extended-surface tubes:
- Fin orientation: Fins run along the tube axis rather than being helically wound. This directs gas flow parallel to the fins, lowering pressure drop and often improving heat transfer in clean service.
- Fin height and channel depth: Fins are tall relative to tube diameter, creating deep channels that compensate for low gas-side heat transfer coefficients.
- Surface treatment: Internal or external surfaces may be treated to support high heat flux duty. The specific treatment varies by manufacturer and project, and must be confirmed against project specifications and manufacturer data.
This product belongs to the broader longitudinal finned tube category and is selected where helical fins would cause unacceptable pressure drop or fouling risk. For comparison designs where pressure drop is not the primary constraint, spiral wound finned tubes may be more suitable. Where compact cross-sections or dirty gas streams are involved, elliptical fin tubes are also candidates.
What Specs, Materials, and Standards Define a High Flux Longitudinal Fin Tube?
Typical specification ranges
| Parameter | Typical range | Unit / note |
|---|---|---|
| Base tube outside diameter (OD) | 25 – 219 | mm |
| Base tube wall thickness | 2.0 – 12.7 | mm |
| Fin height | 10 – 50 | mm, relative to tube diameter |
| Fin thickness | 1.0 – 3.0 | mm |
| Fin count per meter | 200 – 600 | fins/m |
| Single tube length | ≤ 25 | m, subject to transport limits |
| Surface area ratio | 5 – 12 | ratio to bare tube outer surface |
All values above are typical ranges. Final specifications must be confirmed against project specifications, engineer approval, and manufacturer data. Do not design directly from the table.
Materials
| Material class | Typical grades | Service conditions |
|---|---|---|
| Carbon steel | ASTM A106 Gr.B, A179, A210 Gr.A1 | Non-corrosive process fluids, flue gas, steam |
| Stainless steel | 304/304L, 316/316L, 321 | Corrosive fluids, high temperature, marine |
| Alloy steel | T11, T22, T5 | High temperature, high pressure, refinery service |
| Copper alloys | CuNi 90/10, 70/30 | Seawater, HVAC&R, condensers |
| Titanium | Gr.2 | Seawater, chloride environments |
Standards
Base tubes are commonly supplied under recognized tube standards such as ASTM A213, ASTM A179, ASME SA179, ASTM A210, or EN 10216-2. Fin production, attachment process, dimensional tolerances, and inspection typically follow the project specification or applicable standard to be confirmed. Unless the purchase order names a specific standard, grade, and inspection level, the manufacturer should state its default practice and obtain written buyer approval before production. Referenced standards are generic examples only; final requirements must be confirmed against project specifications and engineer approval.
How Do You Calculate Heat Flux, and Why Does It Affect Tube Performance?
Heat flux is the heat transferred per unit area per unit time. It determines tube wall temperature, fin temperature, and whether the heat transfer surface stays within design limits.
The basic heat flux formula is:
Where:
- q″ is heat flux in W/m² or kW/m²
- Q is total heat transfer rate in W
- A is the reference heat transfer area in m²
Reference-area caution: Manufacturers define q″ differently. Some use bare tube outside surface area; others use total extended surface area. Confirm which reference area is used before comparing data from different sources. Mixing references produces misleading comparisons.
For a longitudinal fin tube, total external surface area can be approximated as:
Where:
- A_base = bare tube external surface area in m²
- N_f = number of fins
- h_f = fin height in m
- L = fin length along the axis in m
Typical heat flux ranges for high flux longitudinal fin tubes in high gas-side duty are 30 to 100 kW/m² on a bare-tube-area basis, with higher values possible for specially treated internal surfaces. These are typical ranges—final design values must be established by detailed thermal calculation and confirmed by the project engineer and manufacturer data.
How does fin efficiency affect performance?
Fin efficiency is the ratio of actual heat transferred to the heat that would be transferred if the entire fin were at the base tube temperature. It matters because fin temperature drops along the fin height; if the fin is too tall or too thin, the fin tip approaches the process gas temperature and contributes little. For steel longitudinal fins under typical industrial conditions, well-designed fin efficiency is in the 85% to 95% range. Copper and aluminum fins reach 90% to 98% due to higher thermal conductivity. These are typical ranges—the project engineer should confirm design values against the specific geometry and fluid conditions.
How Is a High Flux Longitudinal Fin Tube Manufactured?
Most high flux longitudinal fin tubes follow this production sequence:
- Material preparation: Base tube and fin strip are traced to heat number. Chemical composition, mechanical properties, and surface condition are checked.
- Tube cutting and cleaning: Base tube is cut to length; surfaces are cleaned of oil and scale.
- Fin forming: Strip is rolled or pressed into longitudinal profiles, with fin height and thickness controlled.
- Attachment: Fins are attached to the base tube along the full length. Common methods include shrink fitting, welding (continuous seam), or integral extrusion. The attachment method determines thermal resistance and mechanical strength.
- Dimensional inspection: Fin height, spacing, thickness, straightness, and total length are verified.
- Surface treatment and marking: Descaling, coating, or blasting as specified; then heat number, material grade, and tube ID are marked at the required location.
- Pressure testing and inspection: Hydrostatic or pneumatic test, plus non-destructive examination as required by the project specification.
The attachment method is critical to performance. A welded or extruded metallurgical bond adds almost no thermal resistance. Mechanical attachment introduces contact resistance at the fin root, reducing fin efficiency. Buyers should specify the attachment method in the purchase order and request inspection records.
How Does a High Flux Longitudinal Fin Tube Compare with a Standard Fin Tube?
| Comparison dimension | Standard longitudinal fin tube | High flux longitudinal fin tube |
|---|---|---|
| Surface area ratio | 3 – 5× bare tube | 5 – 12× bare tube |
| Typical heat flux | Up to 30 kW/m² | 30 – 100 kW/m² and above |
| Fin efficiency | 70% – 85% | 85% – 95% |
| Gas-side pressure drop | Low – moderate | Low – moderate (depends on channel depth) |
| Fouling resistance | Good | Good; deep channels assist self-cleaning |
| Footprint | Baseline | Often smaller for the same heat duty |
| Relative cost | Baseline | Higher per unit length; may be offset in compact units |
Values are typical ranges. Actual performance depends on specific geometry, fluid conditions, cleanliness, and manufacturer data.
How Do You Weigh Fin Density, Pressure Drop, and Fouling Resistance?
Designing a high flux longitudinal fin tube requires balancing three factors that pull against each other. Changing one affects the other two.
- Fin density vs. pressure drop: More fins increase surface area but narrow the flow channels and raise friction pressure drop. Higher pressure drop increases fan or pump power and may require larger rotating equipment.
- Fin height vs. fin efficiency: Taller fins add surface area but the fin tip temperature approaches the gas temperature, lowering efficiency. Beyond a certain point, additional fin height produces diminishing thermal benefit.
- Fin spacing vs. fouling resistance: Wider spacing reduces ash and deposit build-up but provides less area extension. For dust-laden flue gas, wider spacing often matters more than maximum surface area.
- Material cost vs. thermal performance: Copper and aluminum conduct heat better than carbon steel but differ in cost and temperature capability. Choosing a higher-conductivity material reduces fin efficiency losses but may not justify the life-cycle cost.
- Space vs. efficiency: A compact design lowers equipment cost and plot space but may require higher pressure drop or more complex fabrication.
Design principle: For fouling service, the tube with the most compact area in clean conditions is not automatically the best choice. Provide the specified duty and cleaning cycle to the manufacturer so the trade-offs can be evaluated properly.
Which Industries Use These Tubes, and What Are the Application Limits?
High flux longitudinal fin tubes are used where heat transfer is a process bottleneck or an economic constraint. Common industries include:
- Power generation: air-cooled condensers, feedwater heaters, turbine oil coolers, flue gas coolers.
- Petrochemical and chemical processing: process heaters, heat recovery steam generators, reactor cooling, sulfur recovery units.
- HVAC and refrigeration: condensers, evaporators, chillers where compactness and reliability matter.
- Waste heat recovery: flue gas-to-air exchangers, economizers, air preheaters.
- Marine and offshore: seawater-cooled heat exchangers, central cooling systems, lube oil coolers.
- Metallurgy and cement: high-temperature gas cooling, furnace heat exchangers.
Selection limits include:
- High dust loading or sticky deposits may require wider fin spacing or a different tube type.
- At very high gas temperatures, differential thermal expansion between fin and base tube materials must be considered.
- Chloride or acid environments require corrosion-resistant alloys selected for the actual concentration and temperature.
- Maximum single tube length is limited by fabrication, transport, and installation.
- If mechanical cleaning is impossible, online cleaning systems or removable header designs become important.
The points above are general considerations. Specific limits must be confirmed with the project engineer and manufacturer.
What Quality Tests Are Performed During Procurement and Delivery?
| Inspection item | What is checked | Typical method / note |
|---|---|---|
| PMI (positive material identification) | Alloy grade matches certificate | Handheld XRF or laboratory analysis |
| Dimensional inspection | OD, wall thickness, fin height, fin thickness, spacing, length, straightness | Calipers, micrometers, dedicated gauges |
| Visual inspection | Surface defects, fin damage, weld quality, marking | Naked eye or magnification |
| Pressure test | Base tube integrity | Hydrostatic or pneumatic test per project specification |
| Fin attachment integrity | Fin-to-tube bond | Dye penetrant, ultrasonic, or destructive sampling per project specification |
| Hardness test | Base metal and heat-affected zone | Portable hardness tester |
| Third-party inspection | Independent witness and reporting | As appointed by buyer (e.g., SGS, BV, TÜV) |
The inspection scope must be written into the purchase order. The table reflects typical ranges; the final inspection list depends on project specifications, engineer approval, and manufacturer data.
How Are These Tubes Packed and Shipped?
- End protection: Plastic caps or wooden plugs protect tube ends and threads.
- Moisture protection: VCI film, desiccant, or vapor-phase inhibitor wrapping for stainless and alloy tubes.
- Bundling and securing: Steel strapping or banding per project specification, with padding at contact points to prevent transport damage.
- Crating: Wooden crates or pallets depending on size and shipping method.
- Marking: Bundle tags and crate marks carry heat number, material grade, size, quantity, and project reference.
- Shipping method: Road, rail, or sea freight selected against length, weight, route, and delivery schedule.
Packing and shipping requirements must be confirmed against the project specification and contract, particularly for long sea transit, multiple handling points, or special cleanliness requirements.
How Does Lordfintube Demonstrate Traceability and Quality?
For high flux longitudinal fin tubes, supplier documentation matters as much as the product itself. Lordfintube provides:
- Material certificates: EN 10204 3.1 MTC or equivalent as required, linked to heat numbers.
- Traceability: Base tube, fin material, and heat number are traceable through fabrication and shipment.
- Available inspections: PMI, hardness, dimensional, pressure testing, and third-party witness inspection.
- Certification: ISO 9001:2015, valid until 2028-08-21.
- Welding and heat treatment records: Where the product involves welding or heat treatment, PWHT records or process recommendations can be supplied with the shipment.
Request the inspection plan and document list for the specific project so the purchase order and quality records match.
Need a high flux longitudinal fin tube matched to your thermal and mechanical requirements? Share your process conditions, flow rates, and cleaning cycle constraints for a specific proposal.
Request a QuoteFrequently Asked Questions About High Flux Longitudinal Fin Tubes
What exactly is a high flux longitudinal fin tube?
A high flux longitudinal fin tube is an extended-surface heat exchanger tube with axial fins arranged along the tube axis, optimized for high heat flux density. "High flux" describes the heat duty per unit area, not a brand or proprietary grade. It enlarges surface area compared with a bare tube while keeping gas-side pressure drop relatively low.
How do you calculate heat flux?
Heat flux q″ = Q / A, where Q is total heat transfer rate in W and A is reference area in m². The result is expressed in W/m² or kW/m². Manufacturers use different reference areas, so always confirm whether q″ is based on bare tube area or total extended area.
Why choose a high flux longitudinal fin tube over a spiral wound fin tube?
Longitudinal fins are preferred where high heat flux duty or strict gas-side pressure drop limits apply. The axial fins guide flow parallel to the fin surface, lowering pressure drop. For applications where pressure drop is not the primary constraint, spiral wound fin tubes may offer a more cost-effective alternative.
How do you balance fin density and pressure drop during design?
Higher fin density increases surface area but narrows the flow channels and raises pressure drop. Select density so the heat transfer gain exceeds the added fan or pump power, and ensure the cleaning cycle can maintain the chosen geometry. Values must be established against project conditions and manufacturer data.
Which materials are commonly used for high flux longitudinal fin tubes?
Typical materials include carbon steel (A106, A179, A210), stainless steel (304/304L, 316/316L, 321), alloy steel (T11, T22, T5), copper alloys (CuNi 90/10, 70/30), and titanium (Gr.2). Selection depends on fluid corrosivity, temperature, pressure, and cost. These are typical ranges; final material must be confirmed by the engineer.
Can these tubes handle fouling service?
Yes, but fin spacing must be increased to reduce ash and deposit build-up. Provide the actual dust loading, particle size, and cleaning method so the manufacturer can select an appropriate geometry. A high flux longitudinal fin tube does not eliminate fouling; it provides a way to manage it. The guidance above is general; specific limits must be confirmed by the project engineer and manufacturer.

