
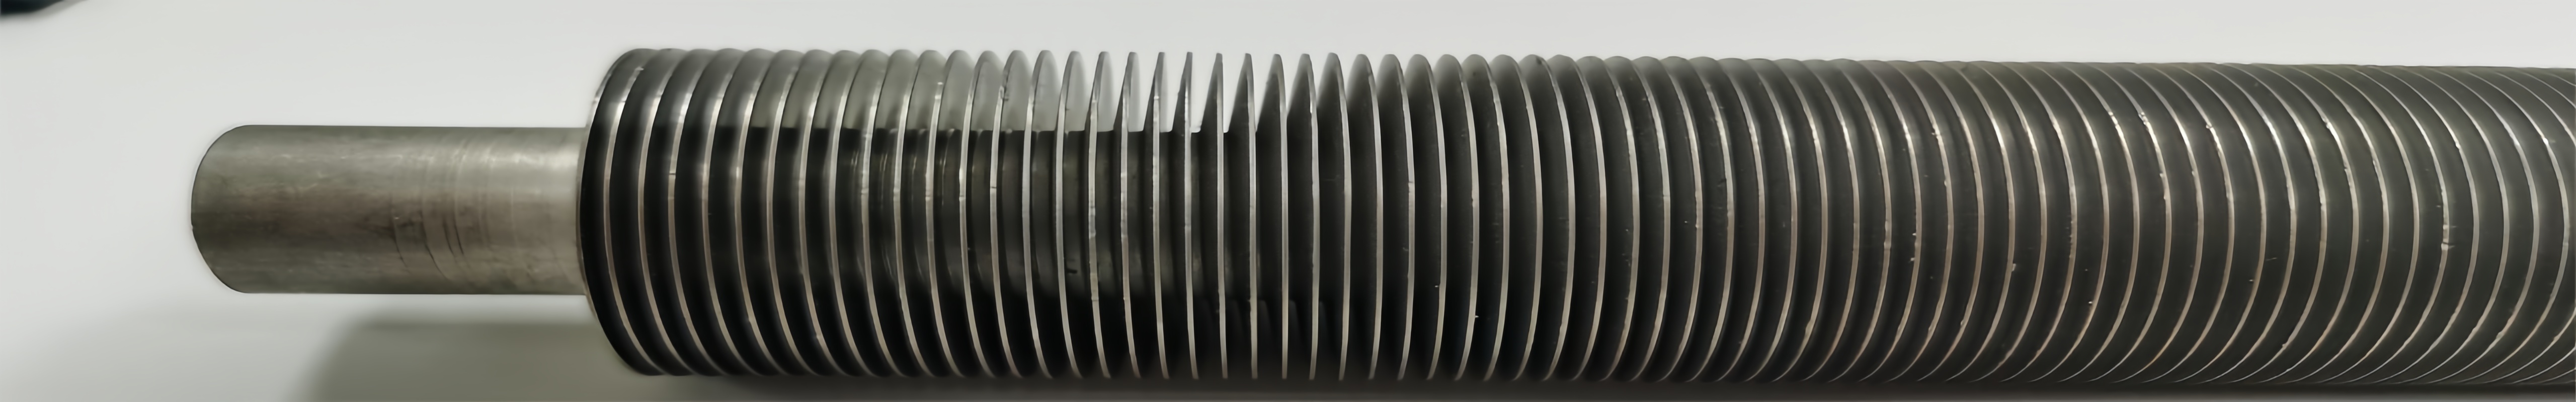
Aluminum Finned Tubes
Aluminum Finned Tubes in Heat Exchange Systems
On the air side of a heat exchanger, the film coefficient is usually an order of magnitude lower than on the tube side. That imbalance, not the tube material, sets the ceiling on how much heat the unit can move. Thickening the tube wall or speeding up the fan only goes so far, so equipment builders expand the surface instead. Aluminum Finned Tubes are one answer to that problem: fins added to the outside of a base tube multiply the area available for convection without enlarging the bundle footprint.
Aluminum earns its place here for several reasons. Its thermal conductivity falls between roughly 200 and 237 W/(m·K) depending on alloy, well ahead of carbon steel. Its density is about one third that of copper, which keeps a finned bundle light enough to hang from a structural frame. It also deforms cleanly, so fins can be wound, embedded or extruded in one pass without cracking at the root. Air coolers, heat recovery trains, heat pumps and process coolers all lean on aluminum finned tubes for these reasons.
Five constructions dominate the market. They differ in how the fin attaches to the tube, and that single difference decides the temperature ceiling, the vibration tolerance and the corrosion behavior of the finished bundle.
How Aluminum Finned Tubes Increase Heat Transfer
The outside area of a finned tube runs 8 to 25 times larger than that of a bare tube of the same length. Three variables drive that ratio: fin height, fin pitch expressed in fins per inch (FPI), and fin thickness. Taller fins add area, and a tighter pitch packs more of them onto each meter of tube.
Area alone does not settle the matter. Fin efficiency describes how closely the fin surface temperature tracks the tube wall temperature. Heat has to travel outward along the fin, so the tip always runs cooler than the root. Tall, thin fins lose efficiency quickly. A design that pushes fin height to the limit can end up with more surface but less useful heat transfer than a shorter, better-balanced fin.
Contact resistance between fin and tube is the other variable that gets overlooked. A wound fin grips by mechanical tension, and repeated thermal cycling can relax that grip over years of service. Embedded and extruded fins form a metallurgical or pressure bond at the root, so the heat path stays intact at higher temperatures and under heavy vibration.
Fin pitch also interacts with the operating environment. Air carrying dust, lint or fibers needs a sparse 4 to 6 FPI layout so the channels stay open and a wash nozzle can reach the tube wall. Clean air allows 8 to 11 FPI, which buys extra area at the cost of higher air-side pressure drop.
| Design Variable | What Changing It Does to Area | Effect on Air-Side Pressure Drop | Where It Pays Off |
|---|---|---|---|
| Fin height, 1/4" up to 1" | Rises with height | Rises | Clean air streams where space is tight |
| Fin pitch, 4 FPI up to 13 FPI | Rises with density | Rises | Dusty air favors 4–6 FPI, clean air 8–11 FPI |
| Fin thickness | Barely changes | Rises slightly | Improves fin efficiency on tall fins |
| Bonding method | No change | No change | Sets the usable temperature and vibration limit |
| Aluminum Property | Typical Value | Why It Matters to the Bundle |
|---|---|---|
| Thermal conductivity | 200–237 W/(m·K) | Keeps the fin tip close to tube wall temperature |
| Density | About 2700 kg/m³ | Reduces bundle weight and support steel |
| Melting point | Around 660 °C | Rarely the limiting factor; the bond fails first |
| Ductility | High in 1050/1100 grades | Allows winding and embedding without root cracking |
Aluminum Finned Tubes Types and Manufacturing
L-Foot Tension Wound Finned Tubes
In this construction the aluminum strip is pre-formed with an L-shaped foot before it is wound under tension around the base tube. The feet overlap each other like roof shingles and cover part of the tube wall, which widens the contact footprint between fin and tube. Nothing is welded and no adhesive is used, so the joint depends entirely on the winding tension.
Because the grip is mechanical, the practical ceiling sits near 300 °F (149 °C). Above that point the aluminum expands faster than the steel tube beneath it and the winding tension falls away, letting fins loosen. In exchange, the shingled foot resists vibration better than a plain edge-wound fin, which is why air cooled heat exchangers and process heaters frequently specify this type.
| Parameter | Specification Range |
|---|---|
| Tube Sizes | 1/2" O.D. to 2" O.D. |
| Fin Heights | 1/4" to 5/8" |
| Fin Pitch | 4 to 13 fins per inch |
| Max. Operating Temperature | 300 °F (149 °C) |
Where it is used
- Air cooled heat exchangers
- Process heaters
- Heat recovery systems
- HVAC coils and air handling units
What the L-foot brings
- Broader tube-to-fin contact than a plain wound fin
- Tolerance of moderate thermal cycling
- Better vibration behavior than edge wound construction
- Low unit cost relative to embedded and extruded types
Edge Tension Wound Aluminum Finned Tubes
Here the strip is wound on edge, meaning the narrow edge of the aluminum band presses against the tube wall. Before winding, the tube surface is knurled so the aluminum bites into fine grooves under pressure. That knurling is what holds the fin in place, and it is the reason this type costs less than the embedded version.
Temperature limits land near 250 °F (121 °C), and vibration tolerance is moderate. Applications with low to moderate heat and modest mechanical movement are the natural fit.
| Parameter | Specification Range |
|---|---|
| Tube Sizes | 1/2" O.D. to 2" O.D. |
| Fin Heights | 1/4" to 1" |
| Fin Pitch | 4 to 13 fins per inch |
| Max. Operating Temperature | 250 °F (121 °C) |
Construction notes
- Knurled tube surface raises the friction between fin and wall
- Fast winding speed keeps production cost down
- Suited to medium temperature duty
- Fin height can reach 1" where extra area is needed
Typical installations
- HVAC and refrigeration coils
- Industrial coolers
- Heat pump evaporators and condensers
- Process cooling circuits
Embedded Aluminum Finned Tubes
Embedded construction starts by plowing a helical groove into the outside of the base tube. The aluminum strip is pressed into that groove, and rolls then close the groove back over the fin root, locking it in place. The fin no longer depends on winding tension, so it survives continuous thermal cycling and high-velocity air streams that would shake a wound fin loose.
The extra machining steps raise the cost above wound types. In return, embedded tubes hold up in power plant air preheaters, chemical process equipment and any duty where vibration is a design concern rather than an afterthought.
| Parameter | Specification Range |
|---|---|
| Tube Sizes | 9/16" O.D. to 2" O.D. |
| Fin Heights | 1/4" to 5/8" |
| Fin Pitch | 5 to 13 fins per inch |
| Max. Operating Temperature | About 400 °F (204 °C) |
Why the embedded root matters
- The mechanical lock holds through repeated heat-up and cool-down
- Contact pressure at the root stays stable over long service
- Heat flows from tube wall into the fin without a shrinking path
- Resists loosening under high air velocity
Where it is specified
- High temperature process heat exchangers
- Power plant air preheaters
- Chemical process equipment
- Ducts and stacks with strong vibration
Extruded Aluminum Finned Tubes
Extruded tubes begin as a thick aluminum sleeve fitted over a liner tube of carbon steel, stainless steel, copper or cupronickel. Rolling pressure squeezes the aluminum outward into fins while pressing the remaining sleeve wall tightly against the liner. Fin and sleeve are one piece of metal, so there is no fin-to-tube contact resistance at all.
That single-piece construction pushes the temperature ceiling to roughly 550 °F (288 °C) and gives the best corrosion performance of the five types, since the aluminum sheath covers the base tube everywhere except the ends. The trade-off is a narrower design window: tube outside diameter is generally limited to 1" through 1 1/4", and fin pitch to 8 through 11 FPI.
| Parameter | Specification Range |
|---|---|
| Tube Sizes | 1" O.D. to 1 1/4" O.D. |
| Fin Heights | 1/2" to 5/8" |
| Fin Pitch | 8 to 11 fins per inch |
| Max. Operating Temperature | 550 °F (288 °C) |
What the extrusion process delivers
- No contact resistance between fin and sleeve
- Stable performance in coastal and chemical atmospheres
- Full aluminum coverage of the base tube along the finned length
- Consistent geometry from tube to tube
Environments that call for it
- Marine and offshore installations
- Chemical plants with corrosive air streams
- High temperature exhaust gas handling
- Outdoor units expected to run for decades
Perforated Aluminum Finned Tubes
Perforated fins are punched with a pattern of holes as the strip passes through the finning machine. The holes sit in a spoke-like arrangement around the tube. They break up the boundary layer that would otherwise cling to the fin surface, letting air reach deeper into the channels between fins. The result is more effective convection and, in many cases, a modest drop in air-side pressure.
Perforated fins can be produced on either an L-foot or an embedded base, so the temperature ceiling follows whichever root style is chosen.
| Parameter | Specification Range |
|---|---|
| Tube Sizes | 9/16" O.D. to 2" O.D. |
| Fin Heights | 1/4" to 1" |
| Fin Pitch | 4 to 13 fins per inch |
| Max. Operating Temperature | Set by the root style (L-foot or embedded) |
Performance gains from the hole pattern
- Higher heat transfer per unit of fin area
- More even air distribution across the bundle face
- Lower air-side pressure drop in many layouts
- Available in several aluminum grades
Where perforated fins fit best
- Compact exchangers with a tight envelope
- Air coolers chasing high efficiency per unit volume
- Retrofit projects with limited fan power
- Duty cycles that reward lower pressure drop
Aluminum Finned Tubes Performance Comparison
| Performance Metric | L-Foot Tension Wound | Edge Tension Wound | Embedded | Extruded | Perforated |
|---|---|---|---|---|---|
| Max. Operating Temperature (°F) | 300 | 250 | 400 | 550 | 300 |
| Vibration Resistance | Excellent | Good | Excellent | Good | Good |
| Corrosion Resistance | Medium | Medium | Good | Excellent | Medium |
| Heat Exchange Efficiency | Good | Good | Excellent | Excellent | Outstanding |
| Cost Effectiveness | High | High | Medium | Low | Medium |
| Fin Pitch Range (FPI) | 4–13 | 4–13 | 5–13 | 8–11 | 4–13 |
| Fin Height Range | 1/4"–5/8" | 1/4"–1" | 1/4"–5/8" | 1/2"–5/8" | 1/4"–1" |
| Typical Duty | General industry | Low and medium temperature | High vibration and heat | Corrosive and high heat | High efficiency layouts |
Performance Comparison of Different Aluminum Finned Tube Types
Relative standing across the combined heat transfer, durability and lifecycle criteria discussed above.
Which Aluminum Finned Tubes Suit Which Conditions
Temperature is the first filter. Below 250 °F, edge tension wound tubes are the cheapest workable option. Between 250 °F and 300 °F, L-foot tubes take over. From 300 °F to 400 °F, the fin has to be locked into the tube wall, which points to embedded construction. Above 400 °F and up to roughly 550 °F, only extruded tubes hold their bond.
Vibration is the second filter. Fans, duct transitions and high-velocity streams all impose cyclic loading on the fin root. Wound fins can work loose under sustained vibration, while embedded and extruded fins keep their grip because the root is captured in metal rather than held by friction.
Corrosion decides the third question. Inland installations with dry air rarely need more than a bare aluminum fin. Coastal sites, pulp and paper plants, and chemical facilities push toward extruded tubes or a coated fin surface.
Finally, the air itself matters. A stream carrying process dust will blind a 13 FPI bundle in months. Dropping to 5 or 6 FPI costs some surface area but keeps the unit cleanable, and that usually wins over the life of the exchanger.
Aluminum Finned Tubes Materials and Standards
Fin stock is normally drawn from the 1050, 1060 or 1100 grades of commercially pure aluminum. These conduct heat well and bend without cracking, which suits winding and embedding. Where more strength or better corrosion performance is needed, 3003 and 6063 alloys come into play.
| Fin Alloy | Thermal Conductivity | Character | Common Use |
|---|---|---|---|
| 1050 / 1060 | About 230 W/(m·K) | Highest conductivity, very ductile | Tension wound fins |
| 1100 | About 220 W/(m·K) | General purpose, easy to form | L-foot and edge wound fins |
| 3003 | About 190 W/(m·K) | Better corrosion resistance, stronger | Embedded and extruded fins |
| 6063 | About 200 W/(m·K) | Good extrusion behavior | Extruded fin sleeves |
Base tubes are supplied in carbon steel, stainless steel 304 and 316, copper, and copper-nickel grades such as 90/10 and 70/30. The pairing of fin alloy and tube material affects both the bond quality and any galvanic risk at the joint, so the two are usually specified together rather than separately.
Fabrication follows recognized material and pressure equipment standards, and most suppliers work under a certified quality management system. Dimensional tolerances on fin height, fin pitch and finned length are worth confirming in writing before production, since small deviations accumulate across a bundle of several thousand tubes.
Material Compatibility
Aluminum fins are wound, embedded or extruded onto carbon steel, stainless steel, copper and cupronickel base tubes.
Thermal Conductivity
Aluminum runs around 200 W/(m·K) or higher, which keeps fin tip temperature close to the tube wall.
Corrosion Protection
Anodizing, epoxy coatings and specialty conversion treatments extend fin life in aggressive atmospheres.
Quality Systems
Production is commonly held to ASTM, ASME and ISO practices for dimensional and performance consistency.
How to Specify Aluminum Finned Tubes
An order that arrives without a full parameter list usually comes back with questions. These are the values a fabricator needs before the finning machine is set up.
- Base tube outside diameter and wall thickness, along with the material grade
- Finned length, bare ends and overall tube length
- Fin height, fin pitch and fin thickness
- Fin bonding method, which sets the temperature and vibration limits
- Fin material grade and any temper requirement
- End treatment, including whether the tube ends are left bare for welding or rolled joints
- Surface finish or coating, if the installation is corrosive
- Acceptance criteria for fin bond, fin pitch tolerance and straightness
Two of these deserve extra attention. Finned length and bare end length should be stated separately, because a bundle that is 20 mm short at each end can fail to seat in the header. And fin pitch should be quoted in fins per inch plus the allowable tolerance, since a nominal 10 FPI bundle delivered at 9.5 FPI loses measurable surface area.
Aluminum Finned Tubes Maintenance and Fouling
Fouling on the air side is the most common reason a finned bundle loses capacity. Dust, pollen and process carryover settle on the fin surface and add a layer of insulation that no amount of fan power can overcome. Because the fin channels are narrow, the deposit builds quickly once it starts.
Dry cleaning with compressed air works for loose deposits. Low-pressure water or a mild detergent wash handles the rest, provided the spray runs parallel to the fins rather than across them. High-pressure jets bend fin edges over, which closes the channels and reduces area permanently.
Fins that have simply been bent can be opened again with a fin comb. A fin that has separated from the tube is a different problem: the original contact pressure cannot be restored by hand, and the usual remedy is to replace the affected tube.
Regular inspection pays off in two ways. It catches fouling before it hardens, and it reveals loose fins or corrosion pitting while the bundle is still worth cleaning rather than replacing.
Aluminum Finned Tubes FAQ
What temperature can aluminum finned tubes handle?
The ceiling is set by the bonding method, not by aluminum itself. Edge tension wound tubes are limited to roughly 250 °F (121 °C), L-foot tension wound to about 300 °F (149 °C), embedded tubes to around 400 °F (204 °C), and extruded tubes to roughly 550 °F (288 °C).
Do aluminum fins corrode in outdoor service?
Aluminum forms a natural oxide layer that slows further attack in most atmospheres. Extruded tubes perform best because the aluminum sheath encloses the base tube almost completely. In coastal, chemical or persistently humid locations, anodizing or an epoxy coating adds years to service life.
How do I choose the fin pitch?
Match the pitch to how dirty the air stream is. Dusty or fibrous air calls for 4 to 6 fins per inch so the channels stay open and can be cleaned. Clean air allows 8 to 13 fins per inch, which raises surface area but also raises air-side pressure drop.
Can damaged aluminum fins be repaired?
Bent fins can usually be straightened with a fin comb. A fin that has come loose from the base tube is harder to restore, because the original contact pressure cannot be recreated by hand. Local replacement of the affected tube is the usual practice.
Can aluminum fins be used on stainless steel or copper tubes?
Yes. Aluminum fins are wound, embedded or extruded onto carbon steel, stainless steel, copper and cupronickel base tubes. What changes between these combinations is the surface preparation and, in some cases, the need for a barrier coating at the joint to avoid galvanic effects.
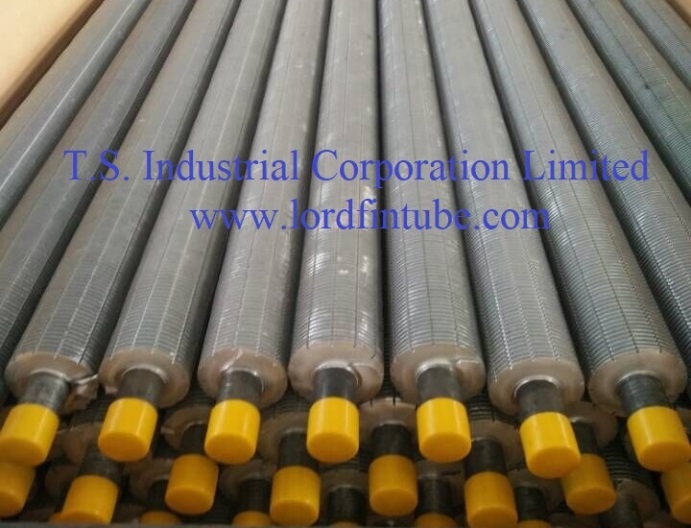
Examples of aluminum finned tubes across the five constructions described above.