
Lord Fin Tube- Extruded Bimetallic Finned Tubes
Extruded Bimetallic Finned Tubes
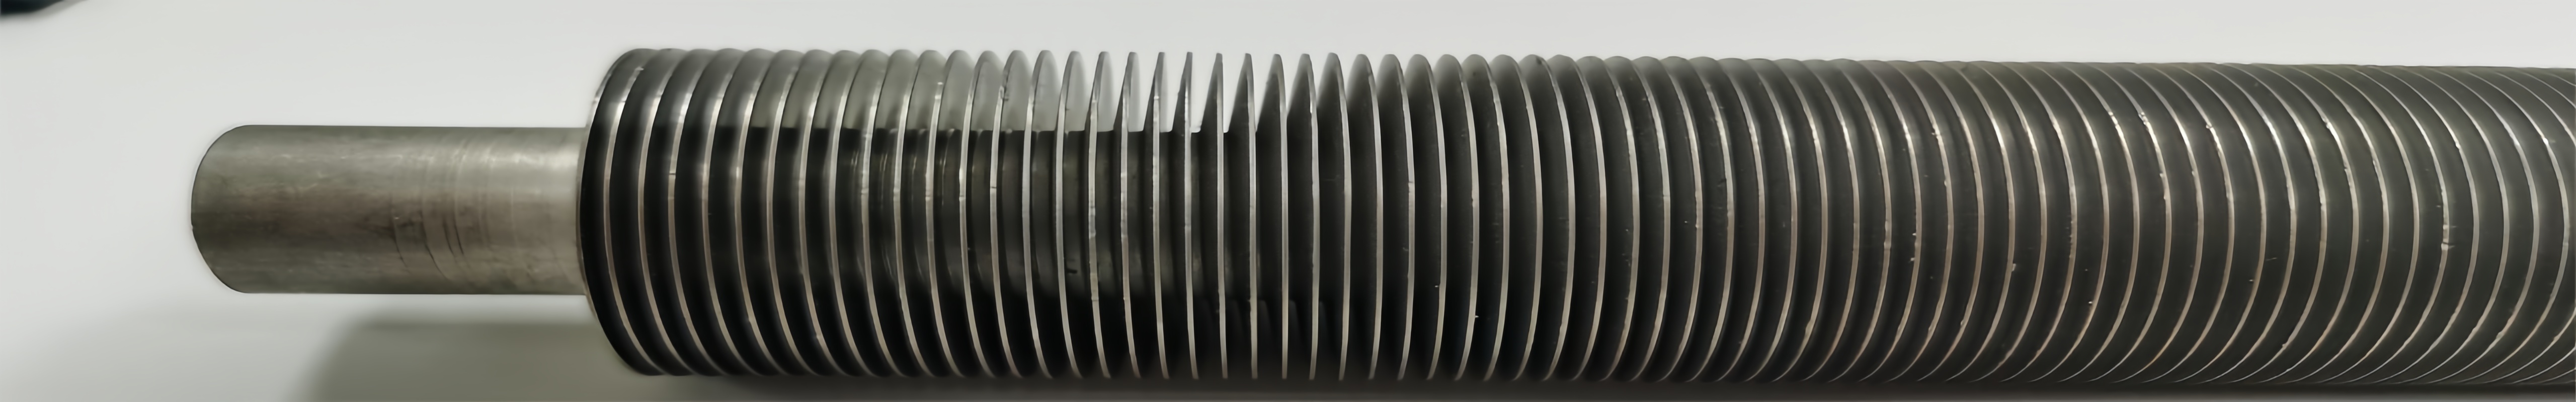
Bimetallic Finned Tubes represent an advanced heat transfer technology where Extruded Bimetallic Finned Tubes are specialized heat exchange elements engineered for optimal thermal performance in demanding applications. These tubes feature a composite structure with two distinct metal layers permanently bonded through an extrusion process.
What distinguishes extruded bimetallic finned tubes from other finned tube types? The metallurgical bond created during extrusion eliminates any thermal contact resistance, allowing heat to flow continuously from the base tube through the fin root to the fin tip. This bond integrity remains stable under thermal cycling, pressure fluctuations, and mechanical vibration — conditions that often cause degradation in mechanically bonded or welded fin designs.
Which industries benefit most from extruded bimetallic finned tubes? Power generation, petrochemical processing, chemical plants, refrigeration systems, marine applications, and natural gas processing all rely on these tubes where reliability and thermal efficiency are non-negotiable. The ability to tailor material combinations — carbon steel, stainless steel, or alloy steel base tubes with aluminum or copper fins — provides design flexibility for specific service environments.
Technical Characteristics
Thermal Conductivity: 180-400 W/m·K (depending on material combination)
Operating Temperature Range: -200°C to +400°C
Pressure Rating: Up to 300 bar (depending on base tube specification)
Fin Efficiency: 85-95% (significantly higher than welded fins)
Bond Strength: >70 MPa (metallurgical bond ensures long-term integrity)
Extruded Bimetallic Finned Tubes Materials
The structural integrity of extruded bimetallic finned tubes derives from the metallurgical bond between the base tube and fin material. This bond ensures optimal heat transfer and mechanical stability under thermal cycling conditions. How does material selection impact overall performance? The thermal conductivity of the base tube and fin material directly influences the overall heat transfer coefficient, while the coefficient of thermal expansion compatibility determines the bonds long-term stability.
Which material combinations are most commonly specified? Carbon steel base tubes with aluminum fins offer the best cost-to-performance ratio for air-cooled applications. For corrosive environments, stainless steel 304 or 316 base tubes paired with aluminum 3003 fins provide excellent resistance to pitting and stress corrosion cracking. When maximum thermal conductivity is required, copper fins on carbon steel or stainless steel base tubes deliver exceptional heat transfer rates.
Material Combinations and Specifications
| Base Tube Material | Fin Material | Thermal Conductivity (W/m·K) | Max Service Temp (°C) | Typical Applications |
|---|---|---|---|---|
| Carbon Steel (SA179, SA210) | Aluminum 1100/3003 | 180-200 | 280 | Air Coolers, HVAC |
| Stainless Steel 304/316 | Aluminum 1100/3003 | 190-210 | 260 | Chemical Processing, Marine |
| Carbon Steel | Copper C12200 | 380-400 | 200 | High Performance Heat Exchangers |
| Stainless Steel 304/316 | Copper C12200 | 390-410 | 180 | Corrosive Environments |
| Alloy Steel (T11, T22) | Aluminum 1100/3003 | 185-195 | 400 | High Temperature Applications |
| Stainless Steel 316L | Aluminum 3003 | 195-210 | 250 | Offshore, Desalination |
| CuNi 90/10 | Aluminum 3003 | 170-185 | 220 | Seawater Coolers |
Base Tube Specifications
OD Range: 12.7mm - 50.8mm
Wall Thickness: 1.2mm - 4.0mm
Length: Up to 24 meters
Materials: Carbon steel, stainless steel, alloy steels, copper-nickel
Fin Specifications
Fin Height: 6mm - 16mm
Fin Thickness: 0.8mm - 2.0mm
Fins per Meter: 200 - 500
Surface Area Ratio: 10:1 - 25:1
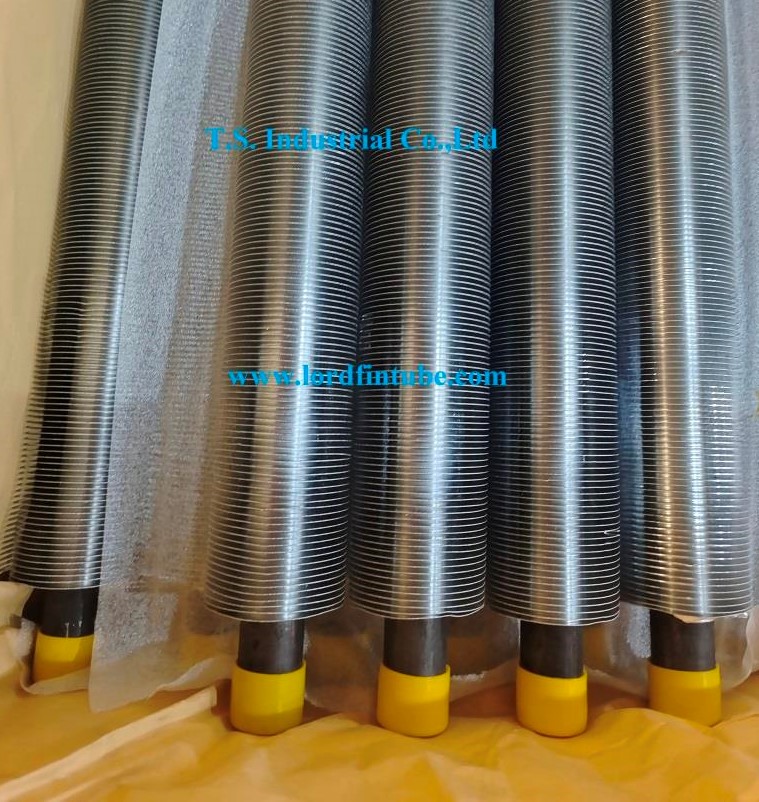
Extruded Bimetallic Finned Tubes - Advanced Heat Transfer Solution
Extruded Bimetallic Finned Tubes Manufacturing Process
The extrusion manufacturing process creates a permanent metallurgical bond between the base tube and fin material, ensuring superior heat transfer characteristics and mechanical integrity. How does the extrusion process achieve this bond? At temperatures between 400-450°C, aluminum atoms diffuse into the steel surface, forming a thin intermetallic layer that provides exceptional bond strength while maintaining thermal conductivity.
Why is the extrusion process preferred over welding for many applications? The continuous bond eliminates the thermal contact resistance found in welded fins, where the weld bead creates a localized heat-affected zone that can become a site for corrosion initiation. Additionally, the extrusion process produces fins with consistent geometry and uniform thickness, ensuring predictable thermal performance across the entire tube length.
Step-by-Step Manufacturing Sequence
| Process Step | Technical Parameters | Quality Control Measures |
|---|---|---|
| Material Preparation | Base tube cleaning to SA2.5 standard Aluminum sleeve thickness: 2-4mm |
Visual inspection, dimensional verification |
| Extrusion Process | Temperature: 400-450°C Pressure: 100-200 MPa Speed: 0.5-2.0 m/min |
Temperature monitoring, pressure control |
| Fin Formation | Die temperature: 200-250°C Fin height tolerance: ±0.2mm |
Optical measurement, sample testing |
| Bond Verification | Bond strength: >70 MPa Thermal cycling: 1000 cycles |
Ultrasonic testing, peel tests |
| Final Inspection | Surface finish check Dimensional accuracy |
Helium leak test, hydrostatic test |
Technical Insight: Metallurgical Bond Formation
The extrusion process creates a true metallurgical bond through controlled intermetallic diffusion. At the optimal temperature range of 400-450°C, aluminum atoms diffuse into the steel surface, forming a thin intermetallic layer (typically 2-5µm) that provides exceptional bond strength while maintaining thermal conductivity.
Which factors influence bond quality? The cleanliness of the base tube surface, the precise control of extrusion temperature, and the uniformity of pressure application all play critical roles. Advanced manufacturing facilities employ real-time monitoring systems to ensure these parameters remain within tight tolerances throughout production.
Extruded Bimetallic Finned Tubes Performance Comparison
Understanding the performance differences between various finned tube technologies is crucial for proper selection in heat exchanger design. What performance metrics matter most? Thermal resistance, fin efficiency, corrosion resistance, maximum operating temperature, and long-term stability all influence the total cost of ownership.
How do extruded bimetallic finned tubes compare to welded fins in real-world operation? Extruded tubes consistently deliver 10-25% higher heat transfer coefficients due to the elimination of contact resistance. Over a five-year service period, extruded tubes maintain 95-98% of original heat transfer capacity, while welded fin tubes typically degrade to 80-90% of initial performance due to corrosion and mechanical fatigue at weld joints.
| Parameter | Extruded Bimetallic | Welded Fins | Integral Low-Fin | Embedded Fins |
|---|---|---|---|---|
| Thermal Resistance | Lowest (0.001-0.003 m²K/W) | Medium (0.005-0.015 m²K/W) | Low (0.002-0.004 m²K/W) | High (0.010-0.025 m²K/W) |
| Corrosion Resistance | Excellent | Good (weld dependent) | Excellent | Fair |
| Fin Efficiency | 90-95% | 70-85% | 85-92% | 60-75% |
| Maximum Temperature | 400°C | 350°C | 450°C | 300°C |
| Cost Factor | 1.0x (Reference) | 0.8x | 1.2x | 0.7x |
| Typical Applications | Corrosive environments, high efficiency | General purpose, moderate conditions | High temperature, high pressure | Light duty, cost-sensitive |
Performance Characteristics
Heat Transfer Performance Comparison
Extended Surface Efficiency: Extruded bimetallic tubes achieve 10-25% higher heat transfer coefficients compared to welded fin alternatives due to the continuous metallurgical bond eliminating contact resistance.
Pressure Drop Characteristics: Optimized fin geometry results in 15-30% lower pressure drop for equivalent heat transfer duty compared to other fin types.
Long-term Performance: After 5 years of service, extruded bimetallic tubes maintain 95-98% of original heat transfer capacity, versus 80-90% for welded fin tubes.
Fouling Resistance: The smooth fin surface and uniform geometry reduce fouling accumulation, extending cleaning intervals by 20-40% compared to welded or embedded fin designs.
Extruded Bimetallic Finned Tubes Application
Extruded bimetallic finned tubes excel in applications requiring superior thermal performance, corrosion resistance, and long-term reliability. Which applications benefit most from this technology? Any heat exchange service where downtime is costly, fluids are corrosive, or thermal efficiency directly impacts operating costs.
Why do engineers specify extruded bimetallic finned tubes for critical services? The combination of high fin efficiency, excellent corrosion resistance, and stable long-term performance makes these tubes the preferred choice for applications where reliability is paramount. The ability to select from multiple material combinations allows designers to match the tube construction to specific process conditions.
- Power Generation - Feedwater heaters, air-cooled condensers, turbine oil coolers
- Petrochemical Industry - Process gas coolers, overhead condensers, reactor feed/effluent exchangers
- Chemical Processing - Acid coolers, solvent condensers, polymerization reactors
- Refrigeration & HVAC - Ammonia evaporators, refrigerant condensers, chiller bundles
- Marine Applications - Seawater coolers, lube oil coolers, central cooling systems
- Natural Gas Processing - Gas dehydration units, amine contactors, glycol coolers
- Waste Heat Recovery - Economizers, waste heat boilers, process gas cooling
- Food & Beverage - Pasteurizers, sterilization systems, process cooling
- Pharmaceutical - Clean steam condensers, solvent recovery systems
- Pulp & Paper - Black liquor evaporators, bleach plant coolers
Industry-Specific Technical Requirements
| Industry | Typical Service Conditions | Recommended Material Combination | Design Considerations |
|---|---|---|---|
| Power Plant Air Coolers | Steam condensation, ambient air cooling Pressure: 5-50 bar, Temperature: 80-200°C |
Carbon Steel / Aluminum | High fin density for maximum surface area, corrosion protection for coastal environments |
| Chemical Process Coolers | Corrosive media, frequent thermal cycling Pressure: 10-100 bar, Temperature: 50-300°C |
Stainless Steel 316 / Aluminum | Enhanced fin thickness for corrosion allowance, optimized for cleaning access |
| Refrigeration Systems | Ammonia or halocarbon refrigerants Pressure: 15-25 bar, Temperature: -40 to +40°C |
Carbon Steel / Aluminum | Optimized for two-phase flow, defrost cycle compatibility |
| Marine Heat Exchangers | Seawater cooling, high corrosion potential Pressure: 5-20 bar, Temperature: 10-90°C |
CuNi 90/10 or 316L SS / Aluminum | Cathodic protection compatibility, enhanced fouling resistance |
| Natural Gas Processing | High pressure gas cooling, H₂S present Pressure: 50-200 bar, Temperature: 20-150°C |
Alloy Steel / Aluminum | Hydrogen-induced cracking resistance, NACE compliance |
Application Engineering
For optimal performance in specific applications, consider the following design parameters:
Air-Cooled Applications: Select fin densities of 394-472 fins/meter (10-12 FPI) with fin heights of 12-16mm for maximum heat transfer efficiency.
Liquid Service: Use lower fin densities of 236-315 fins/meter (6-8 FPI) with optimized fin geometry to minimize fouling and facilitate cleaning.
Corrosive Environments: Specify protective coatings or select appropriate material combinations to ensure 20+ year service life in aggressive chemical services.
Vibration-Prone Installations: Consider fin thickness and root geometry enhancements to resist fatigue failure in high-vibration environments.
The advanced manufacturing process of extruded bimetallic finned tubes ensures a permanent metallurgical bond that provides superior heat transfer efficiency, exceptional corrosion resistance, and long-term reliability in demanding industrial applications.
Extruded Bimetallic Finned Tubes Quality Control
Quality assurance for extruded bimetallic finned tubes involves multiple inspection and testing stages throughout the manufacturing process. What quality standards apply to these tubes? Manufacturers typically comply with ASME Section VIII, TEMA, and ASTM specifications, with additional requirements based on customer specifications and industry codes.
How is bond integrity verified? Non-destructive testing methods including ultrasonic inspection, eddy current testing, and radiographic examination detect any bond imperfections or internal defects. Peel tests and metallographic examination provide destructive verification of bond quality on sample pieces.
Quality Assurance Protocols
| Test/Inspection | Method | Acceptance Criteria | Frequency |
|---|---|---|---|
| Dimensional Verification | Optical measurement, gauge inspection | Fin height ±0.2mm, fin spacing ±0.1mm | 100% of production |
| Bond Integrity | Ultrasonic testing (UT) | No delamination, bond strength >70 MPa | Every tube |
| Hydrostatic Test | Water pressure test | No leakage at 1.5x design pressure | Every tube |
| Peel Test | Destructive sampling | Continuous aluminum layer remains bonded | Per heat/lot |
| Thermal Cycling | Cyclic temperature exposure | No bond degradation after 1000 cycles | Type test per design |
| Corrosion Test | Salt spray, acid immersion | No pitting beyond acceptable limits | Per material combination |
Certifications and Standards
ASME Code: Section VIII, Div. 1 for pressure vessel applications
TEMA Standards: Class R, C, and B for heat exchanger manufacturing
ASTM Specifications: A179, A210, A213, A269 for base tubes; B221 for aluminum fins
ISO 9001: Quality management system certification
NACE Compliance: MR0175/ISO 15156 for sour service applications