
What are the advantages of Painted Finned Tube?
What a painted finned tube carries on its surface
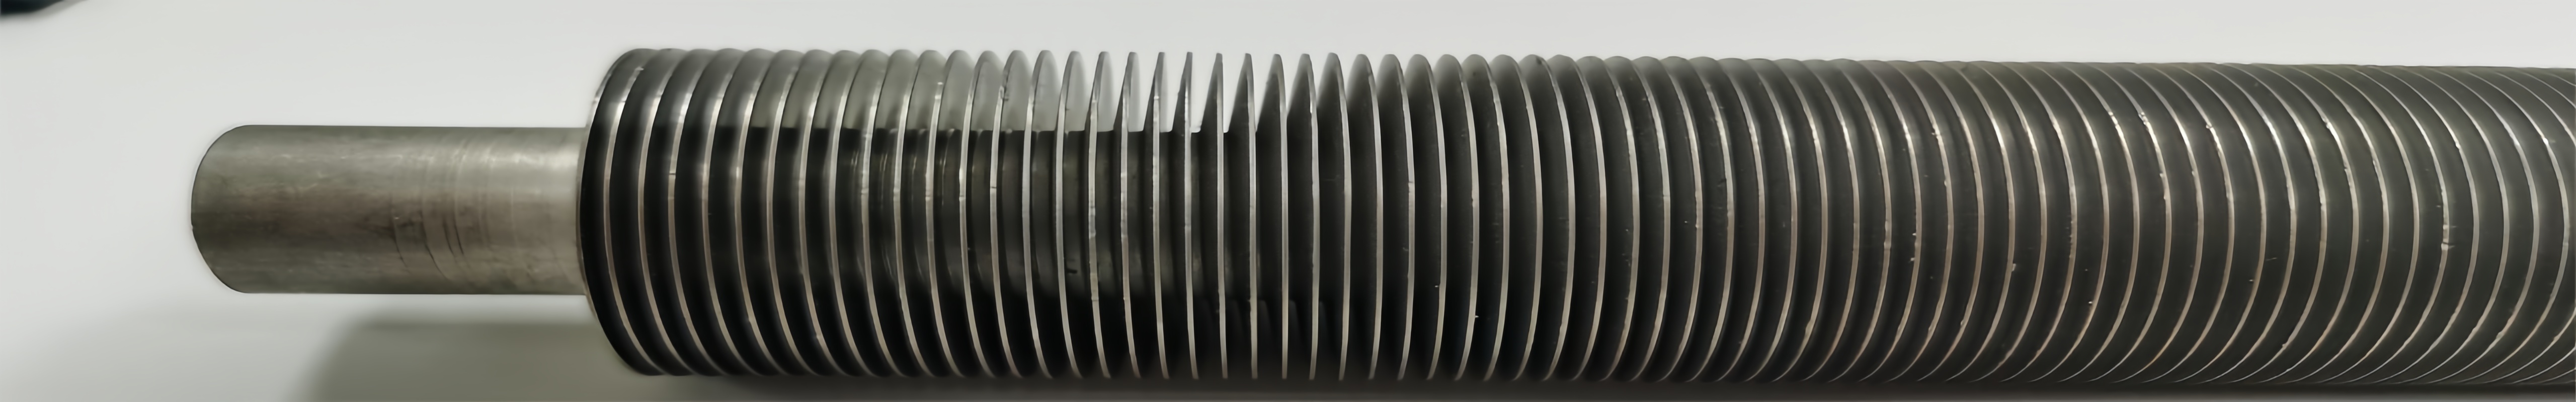
A painted finned tube is built in a fixed order: the fins are attached to the base tube first — by high frequency welding, extrusion, wrapping or embedding — and only then does the whole assembly receive a protective coating. The paint film follows every fin flank, bridges the joint where the fin meets the tube wall, and runs out to the bare ends of the tube.
That order matters more than most people expect. Coating a tube before the fins go on leaves the fin root exposed, because welding or extrusion burns the film away at the joint. The root is exactly where condensate collects and where corrosion starts. Coating after finning covers the joint instead of sacrificing it.
Where the word "paint" misleads people
Industrial fin tube coating has almost nothing in common with the wall paint sold in a hardware store. It is a formulated system of resin, pigment, solvent and curing agent, applied in one or two passes and cured at a controlled temperature. Dry film thickness usually lands between 25 µm and 60 µm. Below that range moisture migrates through; above it the film can crack along the fin edges as the tube cycles between hot and cold. Which system gets used depends on what the tube bundle will actually touch — coastal air, flue gas, steam or chilled water.
Why humid air pushes people toward painted finned tube
Water vapour and acid gas attack the fin root first
On the air side of a fin bundle, condensation gathers between closely spaced fins and carries dust and acid gas down onto the metal. The fin-to-tube joint behaves like a narrow gap, and liquid sits in it far longer than it sits on an open fin surface. Without a barrier, carbon steel forms red rust at that joint while aluminium fins develop white oxide patches. A cured film seals the gap and keeps the liquid on the outside, where airflow can dry it.
Two different metals in contact create a galvanic cell
Aluminium fins wrapped around a carbon steel or stainless tube form a small battery. As soon as a thin electrolyte film connects the two metals, the less noble one starts to dissolve. Because the cured film does not conduct electrons, it interrupts that circuit and slows the galvanic reaction to a crawl. This is one of the least discussed reasons why fin tubes in mixed-metal construction are specified with a coating rather than left bare.
| What is compared | Bare fin tube | Painted fin tube |
|---|---|---|
| First rust spots in coastal air | Often within 6–12 months at the fin root | Usually no rust at the root; slight colour shift on fin tips |
| Galvanic action (aluminium fin on steel tube) | Starts as soon as moisture bridges the joint | Blocked while the film stays intact |
| Air-side heat transfer | Reference value | Roughly 1–3 % lower |
| Cleaning interval | 3–6 months | 6–12 months |
| Service life in a moderately corrosive plant | 3–5 years | 7–12 years |
How painted finned tube changes the heat path
The film adds resistance, but a small amount
Every coating layer resists heat flow. An epoxy film conducts heat at roughly 0.2 W/(m·K), so a 50 µm layer contributes about 0.00025 m²·K/W. On the air side of a finned bundle the convective film coefficient normally sits between 30 and 60 W/(m²·K), which equals 0.017 to 0.033 m²·K/W. The coating therefore adds somewhere near 1 % to 2 % to the dominant air-side resistance — small enough that most thermal designs absorb it without changing the bundle geometry.
Less fouling usually pays back more than the film costs
Fouling is the larger variable. A scale layer conducts heat at 0.5 to 2 W/(m·K), so it only takes about 0.5 mm of deposit to add more resistance than the paint film ever will. A smooth, non-stick surface holds fin spacing open longer, keeps dust from binding to the metal, and lets wash water carry deposits away. Over a full operating year, a painted bundle often delivers a steadier heat duty than a bare one that has quietly fouled.
Surface preparation that decides painted finned tube adhesion
Blasting and degreasing
Adhesion is a mechanical and chemical bond, and it starts long before the spray gun. Tubes and fins are degreased to remove drawing oil and welding residue, then abrasive blasted to Sa 2.5 with a surface profile of about 40–70 µm. The blasted surface is coated within a few hours, before flash rust appears on it. Skipping the profile step is the single most common reason a coating peels off in sheets two winters later.
Primer, topcoat and curing
A zinc phosphate or epoxy primer goes on first to grip the metal and provide a second line of defence if the topcoat is scratched. The topcoat supplies colour, gloss and weather resistance. Curing is controlled: air drying for alkyd systems, or a bake at 120–180 °C for 20 to 40 minutes for thermosetting systems. After curing, adhesion is checked by cross-hatch and mandrel bend tests, and film thickness is measured on fin tips, fin roots and the plain tube ends, because thickness varies across those three zones.
Matching painted finned tube to the right coating
| Coating system | Cure method | Continuous service temperature | Where it fits |
|---|---|---|---|
| Alkyd enamel | Air dry | Up to about 80 °C | Indoor radiators, HVAC coils, decorative convectors |
| Two-component epoxy | Air dry or low bake | Up to about 120 °C | Air coolers, condensers, coastal cooling towers |
| Phenolic / epoxy phenolic | Bake | 150–180 °C | Flue gas heat recovery, air preheaters |
| Silicone aluminium | Bake | 400–600 °C | Boiler economisers, stack gas sections |
Choosing the wrong column is expensive. A phenolic bake applied to an indoor radiator wastes money on curing the plant never needs; an air-dried alkyd put into a 150 °C flue gas stream will chalk, crack and fall off within a season. Temperature, condensate chemistry and the presence of abrasive dust are the three questions that narrow the choice.
Where painted finned tube was used in a real project
At a chemical park on the Zhejiang coast, a waste heat recovery air preheater had been running for years with bare high frequency welded fin tubes. Flue gas left the process at about 160 °C and carried sulphur dioxide plus a heavy moisture load, and the tube bundles were replaced roughly every two years because of rust at the fin roots and blocked fin gaps.
For the 2022 rebuild, the operator switched to carbon steel tubes with high frequency welded steel fins — 32 mm base tube, 12.7 mm fin height, 4 mm fin pitch — finished with a baked epoxy phenolic coating at 40 µm dry film thickness. Ninety-six tubes in four rows were installed in March 2022.
During the planned shutdown in May 2024, inspectors found the film intact across the fin flanks, only slight discolouration on the leading fin tips, no red rust at the roots and no white oxide on the welded joints. Because the fin gaps had stayed clear, gas-side pressure drop was still within 8 % of the commissioning value. A spare bundle from the same supplier, left uncoated and stored outdoors on site, showed rust pitting on the fin roots after about fourteen months of exposure.
The coating added roughly 4 % to the bundle cost. Against a replacement interval that moved from two years to a projected six or more, the plant recovered that difference before the first inspection was due.
What to write on a painted finned tube order
- Base tube material, wall thickness, and fin material, fin height and fin pitch
- Finning method — high frequency welded, extruded, wrapped or embedded
- Coating system name, dry film thickness range and target colour
- Curing schedule the supplier must follow, and whether a bake certificate is required
- Adhesion test method plus any salt spray hours the coating must survive
- Protection during shipping, since strapping and edge contact damage film faster than service does
- Whether tube ends stay uncoated for welding or rolling into the header
Painted finned tube questions that come up most
Does the coating reduce heat transfer noticeably?
It reduces it slightly. A 50 µm film adds about 0.0002 to 0.0003 m²·K/W to the air side, which is around 1 % to 3 % of the total air-side resistance. Because the coated surface also fouls more slowly, a painted bundle usually holds its rated duty longer between cleanings than a bare one.
How hot can a painted finned tube run?
It depends entirely on the resin. Alkyd systems are limited to roughly 80 °C, epoxies to about 120 °C, baked phenolics to around 180 °C, and silicone aluminium systems to 400 °C and above. Above the rated limit the film degrades rather than simply wearing away.
What causes coating to flake off?
Flaking almost always traces back to surface preparation or film thickness. A surface that was not blasted to the required profile, a film laid on too thick at the fin edges, or a cure temperature that was missed by 20 °C will all show up as peeling within a couple of thermal cycles.
Can an existing bare bundle be coated later?
Yes, provided the fins are not crushed or heavily rusted. The bundle has to come out of service, be chemically cleaned and blasted, then sprayed and baked. Touch-up painting on site rarely reaches the fin roots, which is where protection is needed most.
Is a painted finned tube always the right answer?
No. In a dry, dust-free indoor installation with no acid exposure, a bare or zinc-plated tube often costs less and performs just as well. The coating earns its place where moisture, salt, acid gas or mixed metals are present.