
ASME SA213 T91 tube |ASME SA213 Gr T91 Boiler Tube
Power stations that run at higher steam temperatures burn less fuel per megawatt hour, and that single economic fact explains why the ASME SA213 T91 tube sits at the centre of so many superheater and reheater orders. What follows covers what the grade actually is, why it survives at 600 °C, how the tube is made and welded, where it is used, and which checks matter before a shipment leaves the mill.
What ASME SA213 T91 Tube Covers in the SA213 Specification
ASME SA213/SA213M is the standard that governs seamless ferritic and austenitic alloy steel tubes for boilers, superheaters and heat exchangers. Inside that standard, T91 is the grade name and its UNS number is K90901. When the same tube is ordered under the ASTM book, the designation becomes A213 T91. Chemistry and tensile requirements are the same in both books; the ASME version adds rules on heat treatment records, test frequency and marking because SA213 is part of the Boiler and Pressure Vessel Code.
Why does a purchase order spell out “ASME SA 213 Gr T91 Boiler Tube” rather than simply “9Cr steel tube”? Because the grade locks down a defined chemistry window, a defined heat treatment window and a defined testing lot. Those three things are what a design engineer uses when calculating allowable stress, and they are what a welding engineer relies on when qualifying a procedure. An ASME SA213 T91 tube ordered to this specification arrives with a traceable heat number and a certificate that matches the code edition used for the design.
Why ASME SA213 T91 Tube Holds Strength at 600 °C
Open a metallurgy report on T91 and the phrase “tempered martensite” appears quickly. What does that mean in practice? When the tube is normalised near 1040–1080 °C and cooled in air, the structure transforms into hard, stressed martensite. Tempering at 730–780 °C then converts that structure into a stable matrix in which very fine MX type carbonitrides are dispersed.
Vanadium and niobium are the elements that build those particles. They dissolve only slightly at service temperature, so they pin the sub grain boundaries and block the dislocation movement that eventually ends in creep rupture. Chromium, held between 8 and 9.5 percent, forms a tightly adherent oxide on the outside surface, which is why wall thinning from steam side oxidation stays predictable even after tens of thousands of hours.
The practical consequence for a boiler designer is straightforward: at 600 °C, T91 carries roughly twice the allowable stress of 2.25Cr-1Mo (T22), which means a thinner wall, a lighter tube bank, lower thermal stress at the header connection and less weld metal to deposit.
Chemistry of ASME SA213 T91 Tube
| Element | Range (%) | What It Does |
|---|---|---|
| C | 0.08–0.12 | Builds strength; kept low so the weld zone stays tough |
| Mn | 0.30–0.60 | Deoxidation and solid solution strengthening |
| P | ≤0.020 | Residual element, restricted to limit temper embrittlement |
| S | ≤0.010 | Residual element, restricted for ductility and weld quality |
| Si | 0.20–0.50 | Deoxidation, contributes to oxidation resistance |
| Cr | 8.00–9.50 | Steam side and fire side corrosion resistance |
| Mo | 0.85–1.05 | Solid solution strengthening, creep resistance |
| V | 0.18–0.25 | Forms fine carbides that resist coarsening |
| Nb | 0.06–0.10 | Grain refinement, carbide former |
| N | 0.030–0.070 | Stabilises the microstructure, adds strength |
| Ni | ≤0.40 | Residual; limited to keep the transformation behaviour predictable |
| Al | ≤0.02 | Deoxidation; capped so it does not consume nitrogen |
Mechanical Properties of ASME SA213 T91 Tube
| Property | Requirement | Where It Is Verified |
|---|---|---|
| Tensile strength | ≥585 MPa | Tensile test per ASTM A370 |
| Yield strength, 0.2% offset | ≥415 MPa | Tensile test per ASTM A370 |
| Elongation in 50 mm | ≥20% | Tensile test per ASTM A370 |
| Hardness | ≤250 HBW | Brinell test per ASTM E10 |
| Flattening and flare | No cracking | Per SA213 forming tests |
Creep rupture strength is what usually decides the wall thickness. Indicative 100,000 hour values for T91 sit near 180 MPa at 500 °C, near 120 MPa at 550 °C and near 68 MPa at 600 °C. Those figures are for preliminary sizing only; the binding numbers always come from the allowable stress tables of ASME Section II, Part D.
Watch point: hardness above the ceiling almost always points to a tempering temperature that was too low. The tube may still pass tensile testing while carrying a heat affected zone that is far more crack sensitive than the design assumed.
How ASME SA213 T91 Tube Is Manufactured
Almost all T91 boiler tube is produced by the seamless route, because a longitudinal weld in a 600 °C pressure part introduces a creep weak point that designers prefer to avoid. A typical sequence runs from electric arc furnace melting, through ladle refining and vacuum degassing, into continuous casting or ingot teeming, then hot working into a hollow shell, followed by cold drawing or cold pilgering to the finished size.
Heat Treatment of ASME SA213 T91 Tube
The heat treatment step is where the grade is really created. Normalising happens between 1040 and 1080 °C, followed by air cooling. Tempering follows between 730 and 780 °C, again with air cooling. Which parameters matter most? Soaking time uniformity, the cooling rate through the martensite range, and furnace atmosphere control to keep decarburisation shallow. A tube that is normalised but cooled too slowly can retain ferrite, and a tube tempered too hot loses the precipitate density that gives T91 its creep life.
Welding ASME SA213 T91 Tube
Welding this grade is a controlled process rather than a routine one. Filler metal is normally ER90S-B9 for gas tungsten arc welding and E9015-B9 for shielded metal arc welding. Preheating between 200 and 250 °C is standard, interpass temperature is held below roughly 300 °C, and the joint is allowed to cool to below about 100 °C before post weld heat treatment so that the transformation to martensite is complete.
- Post weld heat treatment at 730–780 °C, with thermocouple placement that reflects the real soak of the joint
- Grinding rather than flame cutting close to the joint, to avoid a locally overheated heat affected zone
- Clean, dry consumables and no moisture pickup, since hydrogen cracking is a known failure mode in 9Cr welds
- Hardness survey across the weld and heat affected zone after heat treatment as a routine acceptance check
Where ASME SA213 T91 Tube Is Used
The grade appears wherever metal temperature sits between roughly 540 and 600 °C and pressure is high enough that wall thickness matters.
- Superheater and reheater tubing in subcritical, supercritical and ultra supercritical coal or biomass boilers
- Fired heater and reformer tubing in refinery and petrochemical units
- Heat recovery steam generator tubes downstream of gas turbines
- Main steam and hot reheat piping in thinner wall sizes
- Concentrated solar power receivers and high temperature thermal storage circuits, where the tube sees cyclic heating rather than steady baseload
Project Case with ASME SA213 T91 Tube
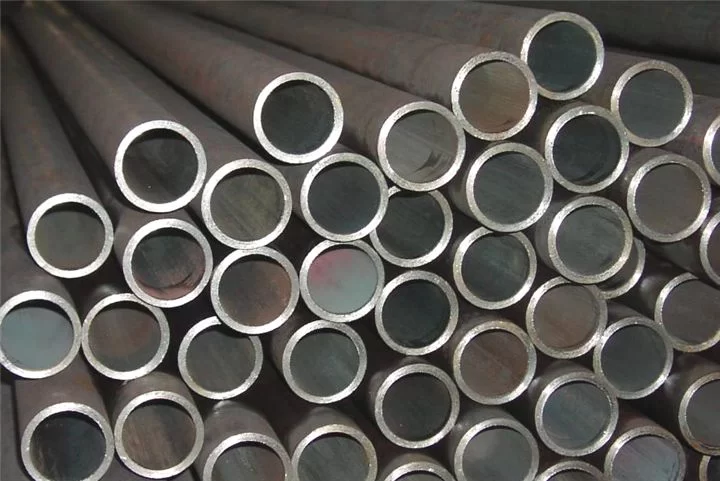
A two by 660 MW ultra supercritical unit built in Southeast Asia needed a final superheater that could hold 605 °C outlet steam at 26.5 MPa. The original design used T22 in the lower temperature passes, but the last two pendant sections were moved to T91 once the allowable stress comparison showed a wall thickness reduction of roughly 25 percent.
| Item | Detail |
|---|---|
| Application | Final superheater pendant tubes |
| Material | ASME SA213 T91, UNS K90901, seamless |
| Size | 45 mm outside diameter × 8.0 mm minimum wall |
| Quantity | Approximately 620 tonnes across two units |
| Supply condition | Normalised and tempered, pickled, ends capped |
| Testing applied | 100% ultrasonic or eddy current, hydrostatic test, tensile and hardness per lot, positive material identification on every length |
| Result | Tube bank weight reduced, header loads lowered, and the unit reached design steam temperature within the first month of commissioning |
What made the order work was not the material alone. It was the agreement up front on heat treatment records, on hardness limits across the weld zone and on the frequency of positive material identification, all of which were written into the purchase specification before the first billet was rolled.
ASME SA213 T91 Tube Compared with T22, T92 and TP347H
| Factor | T91 | T22 | T92 | TP347H |
|---|---|---|---|---|
| Nominal chemistry | 9Cr-1Mo-V-Nb | 2.25Cr-1Mo | 9Cr-2W-V-Nb | 18Cr-10Ni-Nb |
| Practical metal temperature | Up to about 600 °C | Up to about 550 °C | Up to about 620 °C | Up to about 650 °C |
| Thermal expansion | Low | Low | Low | High |
| Thermal conductivity | Good | Good | Good | Lower |
| Weldability | Requires preheat and PWHT | Straightforward | Requires tight control and PWHT | Straightforward |
| Relative material cost | Moderate | Low | High | High |
Checks on ASME SA213 T91 Tube before Shipment
| Check | Method | Frequency |
|---|---|---|
| Grade verification | Optical emission spectrometry or portable XRF | Every length |
| Dimensions | Micrometer and ultrasonic wall measurement | Every length |
| Internal soundness | Eddy current or ultrasonic testing | Every length |
| Pressure integrity | Hydrostatic test | As specified on the order |
| Tensile and hardness | ASTM A370 and ASTM E10 | Per lot |
| Microstructure | Metallographic examination for tempered martensite | Per lot or per heat |
| Decarburisation depth | Metallographic measurement | Per heat |
Two documents decide whether a T91 shipment is usable: the heat treatment record with real chart data, and the hardness survey across any welded test coupon. Certificates that list only chemistry and tensile results leave the most likely failure mode unverified.
Questions about ASME SA213 T91 Tube
Is ASME SA213 T91 the same material as ASTM A213 T91?
The chemistry and tensile requirements are identical. SA213 is the ASME Boiler and Pressure Vessel Code edition of the same specification, so it carries additional rules on heat treatment records, test frequency and marking. For a stamped pressure part, SA213 is normally the version that must appear on the mill certificate.
What is the difference between ASME SA213 T91 and T92 tube?
T92 replaces part of the molybdenum with 1.5 to 2.0 percent tungsten and lowers molybdenum to roughly 0.3 to 0.6 percent. That change lifts the usable metal temperature to about 620 °C and improves creep rupture strength, but T92 costs more and demands tighter welding control, so T91 remains the default choice up to about 600 °C.
Does ASME SA213 T91 tube need post weld heat treatment?
Yes. Welded T91 joints are normally given post weld heat treatment between 730 and 780 °C after the weld has cooled below the martensite finish temperature. Skipping this step leaves a hard, brittle heat affected zone and is one of the most common causes of early cracking in superheater tube welds.
Why is the hardness of T91 tube limited?
A hardness ceiling of about 250 HBW keeps the tempered martensite from becoming too brittle. Tube that is over hardened usually means the tempering temperature was too low or the cooling after normalising was uneven, and it will show poor impact toughness and poor stress rupture behaviour in service.
What size range is available for ASME SA 213 Gr T91 Boiler Tube?
Cold drawn seamless T91 tube is commonly produced from about 6.35 mm outside diameter up to 114.3 mm, with wall thickness from roughly 0.9 mm to 15 mm. Larger diameters and heavier walls are usually supplied as hot finished or as forged and bored product.
When should TP347H be selected instead of T91?
Austenitic grades such as TP347H are preferred when metal temperature stays above roughly 620 °C, or when the flue gas carries aggressive sulphur and chlorine species that attack the protective chromium oxide layer. T91 still wins on thermal expansion and heat transfer, so the decision is usually about temperature and corrosion rather than price alone.