
Custom Furnace Convection Coils for Petrochemical Heaters
Advancing Heat Recovery in Fired Heaters Industrial fired heaters and process furnaces operate under demanding thermal environments where maximizing heat transfer is directly tied to operational profitability. While the radiant section captures direct flame heat, the furnace convection coil positioned in the upper flue gas path plays a critical role in reclaiming residual thermal energy. Lord Fin Tube has upgraded its specialized fabrication lines to deliver precision-engineered convection coil assemblies tailored for petrochemical refineries, chemical processing plants, and power generation facilities worldwide. By enhancing heat absorption from high-temperature flue gases, these custom coils significantly improve overall thermal efficiency and reduce fuel expenses.
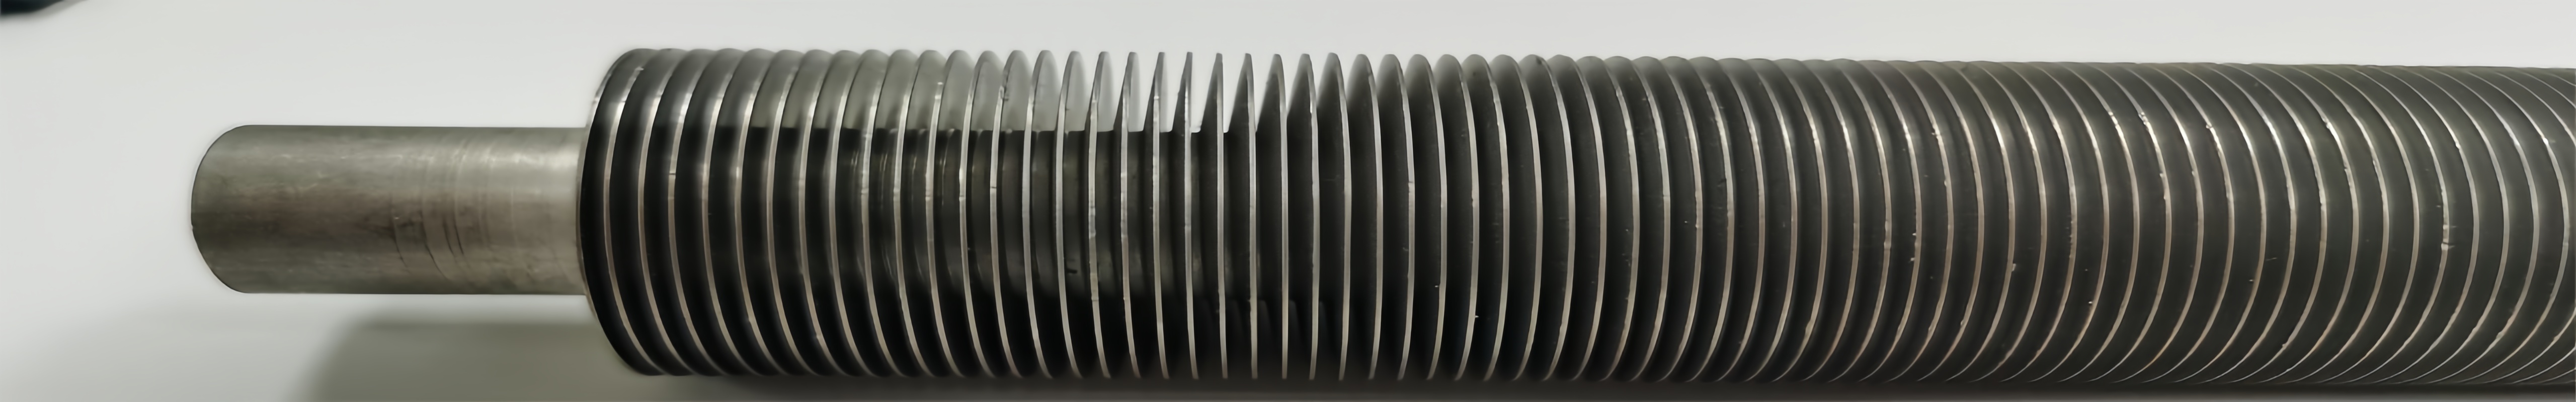
Engineering Designs for Diverse Flue Gas Conditions Flue gas compositions vary dramatically depending on the fuel source, ranging from clean natural gas to heavy residual oils containing high levels of sulfur and particulates. Selecting the correct extended surface geometry is essential to prevent fouling and ensure long-term structural integrity. Lord Fin Tube manufactures convection coils utilizing multiple fin configurations. High-frequency solid and serrated finned tubes are engineered for clean-burning gas applications, providing a dense heat transfer surface area within a compact footprint. Conversely, for heavy oil-fired heaters prone to soot accumulation, studded tubes are fabricated with precision-welded cylindrical or elliptical studs that withstand aggressive soot-blowing operations and corrosive exhaust environments.
Metallurgical Excellence and Material Selection Operating temperatures in convection zones frequently exceed 500°C to 800°C, subjecting pressure-retaining components to severe oxidation, creep, and thermal fatigue. To meet rigorous international standards such as ASME and ASTM, Lord Fin Tube sources certified base tubes and fin strips across a comprehensive spectrum of alloys. Standard carbon steels including ASTM A106 Gr.B and A335 P11/P22 alloy steels serve mid-to-high temperature zones, while austenitic stainless steels such as TP304H, TP316L, and TP347H are deployed in corrosive or extreme-heat shock rows. Every metallurgical pairing is carefully verified to ensure compatible thermal expansion coefficients between the base tube and the welded fin or stud.
Precision Fabrication and Custom Coil Assembly A complete furnace convection coil requires far more than individual finned tubes; it demands exact dimensional accuracy across multi-row serpentine bundles, U-bends, headers, and intermediate tube sheets. At the Lord Fin Tube manufacturing facility, automated high-frequency resistance welding ensures a continuous, metallurgical bond with minimal thermal resistance at the fin-to-tube interface. Following finning, tubes undergo precision cold or hot bending to achieve tight bend radii without wall thinning beyond code tolerances. Experienced ASME-certified welders then assemble the U-bends, return headers, and alloy tube supports, ensuring seamless drop-in alignment during client plant turnarounds and revamps.
Technical Specifications and Customization Capabilities To support diverse EPC contractor requirements and OEM heater designs, Lord Fin Tube offers extensive customization parameters for convection section modules: Base Tube Outside Diameter: 25.4 mm to 219.1 mm (1 inch to 8 inches) Base Tube Wall Thickness: 2.5 mm to 18.0 mm, compliant with ASME SA106, SA213, SA335, and SA312 Fin Types: Solid helical fins, serrated helical fins, and resistance-welded studs Fin Materials: Carbon steel, Corten steel, 11-13% Cr ferritic steel (TP409/TP410), and 300-series stainless steels Fin Density and Height: Fin pitch from 40 to 280 fins per meter; fin height from 8 mm to 32 mm Assembly Configurations: Multi-pass serpentine coils, hairpin bundles, and complete modular convection boxes with refractory-lined casings and structural steel frames
Stringent Quality Assurance and Non-Destructive Testing Reliability in high-pressure process heaters is non-negotiable, as a single tube failure can force a costly unscheduled plant shutdown. Every furnace convection coil produced by Lord Fin Tube undergoes a comprehensive inspection protocol prior to dispatch. Quality control measures include positive material identification (PMI) on all alloy components, tensile destructive testing of fin weld bonds, radiographic testing (RT) and ultrasonic testing (UT) of pressure-retaining butt welds, and liquid penetrant testing (PT) on critical bend areas. Hydrostatic pressure testing is conducted on completed coil assemblies to verify leak-free integrity under design pressures.
Global Export Logistics and Project Support Plant revamps and scheduled maintenance turnarounds operate on strict timelines where delayed deliveries are not an option. Lord Fin Tube coordinates end-to-end export packaging and logistics to protect delicate finned surfaces and heavy header structures during ocean transit. Coils are secured in custom-built steel-wood composite frames with moisture-barrier wrapping and internal bracing to prevent transit deformation. Engineering teams provide full bilingual documentation, including mill test certificates (EN 10204 3.1), welding procedure specifications (WPS/PQR), and dimensional inspection reports.
Partnering for Long-Term Thermal Performance Upgrading an aging convection section or specifying coils for a new fired heater requires a manufacturing partner with proven metallurgical knowledge and heavy fabrication capacity. Procurement managers and thermal engineers seeking reliable, custom-built furnace convection coils can review detailed technical datasheets and submit project drawings directly through the official website at