
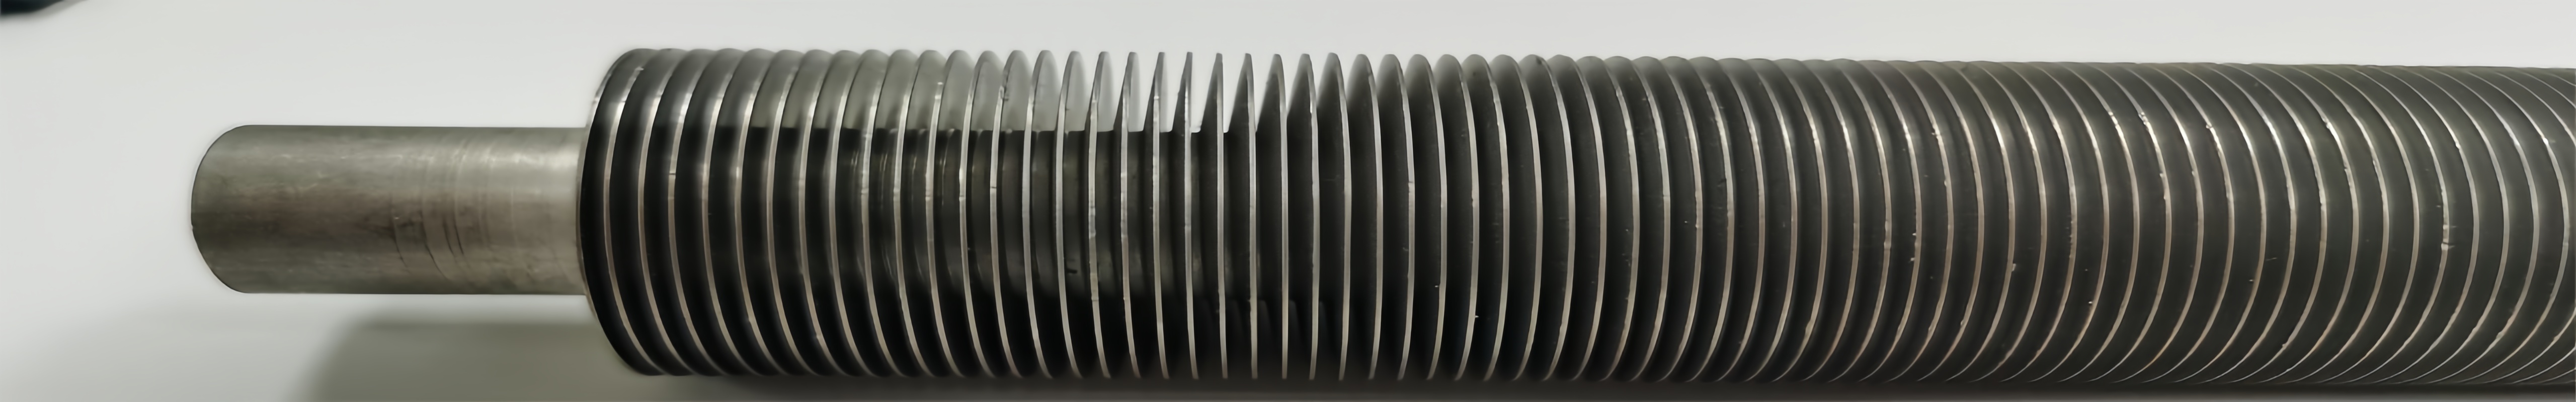
SA335 P11 SS409 HFW Finned Pipe|HFW SA335 P11 Fin Pipe
The SA335 P11 SS409 HFW (High-Frequency Welded) Finned Pipe combines a high-temperature-resistant SA335 P11 chromium-molybdenum alloy steel base pipe with corrosion-resistant SS409 stainless steel fins, utilizing advanced high-frequency welding technology to create a durable, efficient heat transfer solution for power plants, petrochemical systems, and industrial boilers operating under extreme temperatures (up to 540°C) and corrosive environments.
What HFW SA335 P11 Fin Pipe Does in Heat Recovery
Heat recovery equipment often faces a basic problem: flue gas carries useful thermal energy, but bare tubes simply do not have enough surface area to capture it efficiently. A SA335 P11 Fin Pipe solves this by attaching fins to the outer wall of a strong alloy tube. The fins multiply the available surface area, so the same tube length transfers far more heat. The base pipe handles pressure and temperature; the fins handle surface area and corrosion resistance. That division of labor is why this product works in places where a single-material tube would fail.
High-Frequency Welded Finned Tubes are high-efficiency heat exchange components where metal fins are securely welded to the outer surface of a base pipe through high-frequency induction welding technology. Their core function is to significantly increase heat transfer surface area, improving thermal conduction efficiency for applications in high-temperature, high-pressure, and corrosive environments.
- Power plants: Boiler economizers, superheaters, air preheaters
- Petrochemical plants: Reboilers, condensers, catalytic cracking units
- Waste heat recovery: Flue gas desulfurization systems, exhaust gas coolers
- Industrial boilers: Waste heat boilers, gas turbine heat exchange modules
How HFW SA335 P11 Fin Pipe Is Made
Making a finned pipe that survives thermal cycling is not just about choosing good materials. It is about how those materials are joined. High-frequency welding uses a current in the 100–400 kHz range. That current concentrates at the contact point between the fin root and the pipe surface, heating the interface to roughly 1200–1300°C in a fraction of a second. The fin root and a thin layer of the pipe surface melt together, and as the current moves on, the weld cools immediately. No filler metal is added. The result is a metallurgical bond rather than a mechanical fit.
Why does this matter to a buyer? A mechanically attached fin—say, a tension-wound or embedded fin—can loosen after thousands of thermal cycles. Once the fin loses contact with the pipe, heat transfer drops and the joint becomes a failure point. A high-frequency weld keeps the fin bonded because the bond is not a press fit; it is a continuous welded seam. Shear strength typically reaches 200 MPa or higher, which is strong enough to survive vibration, thermal expansion, and handling during installation.
Another advantage is the heat-affected zone. Because heating is localized and brief, the zone stays under about 1 mm. That means the SA335 P11 base pipe does not lose its heat treatment or creep resistance near the weld. The pipe performs as if it were still a plain tube, and the fins perform as if they were part of it.
Which Materials HFW SA335 P11 Fin Pipe Uses
SA335 P11 Base Pipe Properties
SA335 P11 is a seamless ferritic alloy steel specified under ASTM A335. It contains chromium and molybdenum, which together provide strength at elevated temperatures and resistance to oxidation. The grade is sometimes compared to Chinese 15CrMoG or German 13CrMo4-5, and it has been used in high-temperature piping for decades. What makes it suitable as a finned pipe base is its combination of creep strength and weldability. It does not become brittle after long exposure at 540°C, and it can be welded to fins without preheating complications when the correct procedure is followed.
| Chemical Composition of SA335 P11 (wt%) | ||||||
|---|---|---|---|---|---|---|
| Element | C | Mn | Si | Cr | Mo | P/S |
| Range | 0.05–0.15 | 0.30–0.60 | 0.50–1.00 | 1.00–1.50 | 0.44–0.65 | ≤0.025 |
| Property | Value |
|---|---|
| Tensile strength (σb) | ≥415 MPa |
| Yield strength (σs) | ≥205 MPa |
| Elongation (δ) | ≥30% |
| 100,000-hour rupture strength at 550°C | ≥80 MPa |
| Typical heat treatment | Normalize at 930°C, temper at 650°C |
Oxidation resistance comes from a chromium oxide layer that forms below 540°C. That layer is stable in combustion gas environments, which is why SA335 P11 is common in boiler tubes and economizers. When welding, preheat to 200–300°C helps prevent cold cracking, and E8018-B2 electrodes are a common match for manual work.
SS409 Fin Properties
SS409 is a ferritic stainless steel with about 11% chromium and a titanium addition that stabilizes carbon. It sits between carbon steel and austenitic stainless steel in both cost and corrosion performance. For fin material, that middle position is often exactly right. Carbon steel fins would rust away in flue gas; 304 or 316 fins would cost significantly more and may not be necessary if the temperature stays within limits.
| Chemical Composition of SS409 (wt%) | |||||
|---|---|---|---|---|---|
| Element | C | Cr | Ti | Mn | Si |
| Range | ≤0.08 | 10.5–11.7 | 6×C–0.75 | ≤1.0 | ≤1.0 |
SS409 resists atmospheric corrosion better than carbon steel but is not immune to chloride attack. In sulfur-containing flue gas, the dew point matters. If the metal surface drops below the acid dew point, condensation can form and attack the fin. Keeping the surface temperature above roughly 400°C in those environments avoids the worst of it. Continuous service temperature for SS409 reaches 650°C, and short-term oxidation resistance extends to about 800°C. That is more than enough for most economizer and heat recovery duties where SA335 P11 is the base pipe.
Fins are typically cold-rolled to heights up to 16 mm with pitches between 3 and 8 mm. Surface treatment such as sandblasting or pickling passivation can improve corrosion resistance further, but it also adds cost. The decision depends on the flue gas composition and the expected service life.
Why SS409 Fins on SA335 P11 Pipe
Not every finned pipe needs a stainless fin. In clean, dry, high-temperature gas, carbon steel fins might last years. But in real plants, flue gas contains sulfur, moisture, and sometimes chlorides. Carbon steel fins corrode, and when they corrode, they lose thickness and eventually detach. SS409 gives a meaningful step up in corrosion resistance without the price jump to austenitic grades.
The pairing also works thermally. SA335 P11 and SS409 have compatible thermal expansion characteristics, so the weld does not experience excessive stress when the pipe heats and cools. If the expansion coefficients were very different, the weld could crack after repeated cycling. That compatibility is not accidental; it is one reason this material combination appears in so many heat recovery specifications.
What to watch: SS409 is not a replacement for 304 or 316 in chloride-rich environments. If the flue gas contains significant chlorides or the operating temperature is low enough for condensation, a higher-alloy fin may be necessary. The base pipe may still be SA335 P11, but the fin material choice should match the corrosion environment.
Where HFW SA335 P11 Fin Pipe Runs in Plants
Project example: 350 MW coal-fired unit economizer replacement, northern China, 2023
A 350 MW coal-fired power plant in northern China replaced the economizer section of a boiler with HFW SA335 P11 finned pipe using SS409 fins. The flue gas inlet temperature at the economizer was 540°C, and the gas contained sulfur compounds typical of bituminous coal combustion. The original bare tube economizer had limited heat recovery because of surface area constraints, and the plant wanted to lower exhaust gas temperature without increasing back pressure.
The replacement used SA335 P11 base tubes with 12 mm high SS409 fins at a 5 mm pitch. After 12 months of continuous operation, eddy current testing showed no fin weld failures. Heat transfer efficiency improved by approximately 18% compared to the previous bare tube design. The plant reported no measurable increase in flue gas pressure drop across the economizer section.
The project demonstrates the practical value of the material combination: SA335 P11 handled the pressure and temperature, SS409 survived the flue gas environment, and the HFW bond kept the fins in place through a year of thermal cycling.
How to Specify HFW SA335 P11 Fin Pipe
Buyers who know what to specify get better pricing and fewer surprises. The table below lists the parameters that matter most. Values shown are typical examples, not fixed requirements. Actual selections depend on the heat transfer calculation, the flue gas conditions, and the mechanical design of the equipment.
| Parameter | What it affects | Typical example |
|---|---|---|
| Base pipe dimensions | Pressure capacity, flow area | Φ38 × 4 mm |
| Fin height | Surface area vs. pressure drop | 12 mm |
| Fin thickness | Wear life, corrosion allowance | 0.8 mm |
| Fin pitch | Fouling tendency, heat transfer | 5 mm |
| Working pressure | Wall thickness calculation | 6.4 MPa (per ASME B31.3) |
| Design temperature | Material selection, creep life | 540°C |
| Fin-to-tube weld shear strength | Mechanical durability | ≥200 MPa |
When the environment is more aggressive than SS409 can handle, options exist. Internal cladding with Alloy 625 protects the inside of the base pipe from corrosive process fluids. Duplex stainless steel fins such as S31803 can replace SS409 where chloride corrosion is a concern. Tungsten carbide coatings on the fin surface extend life in ash-heavy or erosive gas streams. Each of these adds cost, so they should be justified by the actual operating conditions rather than applied by default.
FAQs About HFW SA335 P11 Fin Pipe
What temperature can SA335 P11 finned pipe handle?
The SA335 P11 base pipe is suitable for continuous service up to about 540°C. The SS409 fins can handle continuous service up to 650°C and short-term exposure to 800°C. The limiting factor is usually the base pipe when pressure is involved, and the fin material when corrosion is involved. For combined high temperature and high pressure, 540°C is the practical upper limit for this material combination.
Why use SS409 fins instead of carbon steel fins?
Carbon steel fins corrode in flue gas containing sulfur and moisture. SS409 resists that corrosion much better because of its chromium content. The cost difference is modest compared to the service life improvement, especially in plants that cannot afford frequent downtime for fin replacement. In clean, dry gas streams, carbon steel fins may be adequate and less expensive, but those conditions are less common in real installations.
How is HFW different from other fin welding methods?
High-frequency welding creates a metallurgical bond without filler metal, with a very small heat-affected zone and high production speed. Other methods include tension winding, which relies on mechanical contact, and embedded welding, which requires a groove in the pipe. HFW produces a stronger bond and less base pipe distortion than most alternatives, and it is well suited to high-volume production of SA335 P11 finned pipe.
What is the typical service life of SA335 P11 SS409 finned pipe?
Service life depends on temperature, flue gas composition, and thermal cycling. In a well-controlled economizer environment with flue gas above the acid dew point, 15 to 20 years is a reasonable expectation. In more aggressive conditions, life may be shorter. Eddy current testing and visual inspection during outages can track fin weld condition and help predict remaining life.
Can SA335 P11 finned pipe be repaired if a fin weld fails?
In most cases, a failed fin weld cannot be repaired in the field to the same strength as the original HFW bond. The practical approach is to monitor fin condition and replace affected sections during scheduled outages. This is another reason to choose the right material combination at the specification stage—a properly selected SA335 P11 SS409 pipe with good weld quality should not need frequent repair.
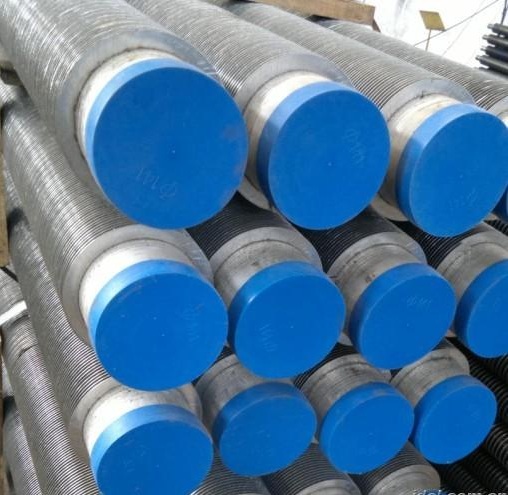
SA335 P11 SS409 HFW Finned Pipe