
Tube standard for fin tube heat exchanger
Published 12 November 2024
Finned Tube Heat Exchanger Composition
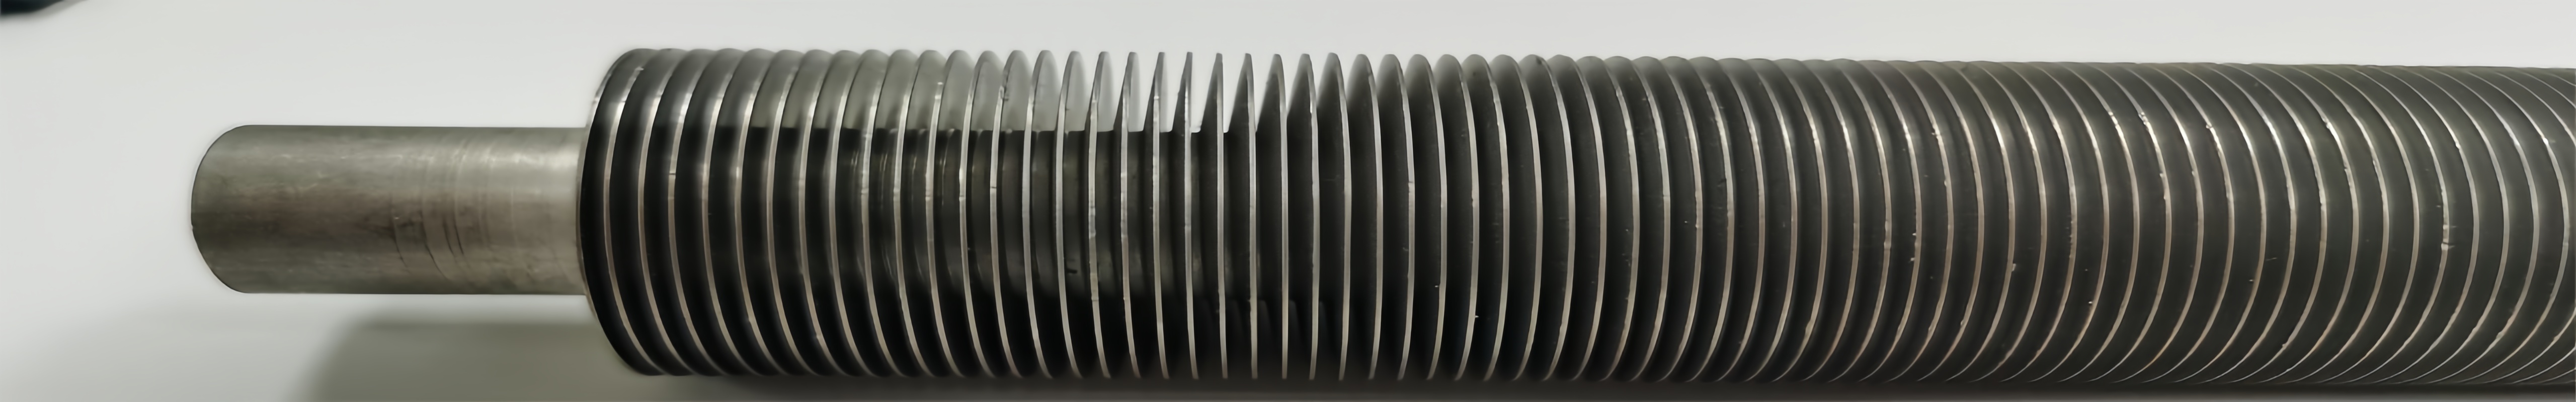
Fin tube heat exchanger is a heat exchanger consisting of finned tube (also known as finned pipe) with supporting structure and shell. Finned tube is the main heat exchanger. Finned tube is composed of base tube and fin. The combination mode includes expansion joint, high-frequency welding, laser welding and so on. Tube-fin heat exchanger is one of the most efficient heat exchangers. It is widely used in many fields, such as power, refrigeration and heating, chemical industry, medicine, food and beverage. Compared with traditional heat exchangers, tube fin heat exchangers have the following characteristics:
- The heat transfer area is greatly increased, which is 2-10 times higher than the heat transfer area of the light pipe, and it is more efficient and energy saving.
- It can promote the formation of fluid turbulence, and the heat transfer coefficient is 1-2 times higher than that of the light tube.
- Compact structure, reduce consumption of metal materials, less space and space.
- The fins can be different from the base materials, and the selection and utilization of materials are more reasonable and economical.
- Long service life, no string liquid, low maintenance cost.
What decides whether those five points actually hold up on site is rarely the fin itself. It is the tube standard behind the base pipe. Two finned tubes can look identical on a drawing and behave very differently after two years in service, depending on whether the base tube was produced to a boiler grade, a general service grade or a sanitary grade. Wall thickness tolerance, weld seam quality, heat treatment and the level of non destructive testing all come from that one line on the purchase order.
Finned Tube Standards by Body and Region
Below is the set of tube specifications most often quoted when a finned tube bundle is being built. Read the list with one question in mind: which of these governs the tube my fins are going onto?
| Standard | Title or scope |
|---|---|
| ASTM A249/A249M | Specification for Welded Austenitic Steel Boiler, Superheater, Heat-Exchanger, and Condenser tubes |
| ASTM A268/A268M | Standard specification for Seamless and Welded Ferritic and Martensitic Stainless Steel Tubing for General Service |
| ASTM A269/A269M, ASME SA269/SA269M | Specification for Seamless and Welded Austenitic Stainless Steel Tubing for General Service |
| ASTM A270 | Specification for Seamless and Welded Austenitic and Ferritic/Austenitic Stainless Steel Sanitary Tubing |
| ASTM A312/A312M, ASME SA312/SA312M | Specification for Seamless and Welded Austenitic Stainless Steel Pipes |
| ASTM A358/A358M | Specification for Electric-Fusion-Welded Austenitic Chromium-Nickel Alloy Steel Pipe for High-Temperature Service |
| ASTM A409/SA409 | Welded Large Diameter Austenitic Steel Pipe for Corrosive or High Temperature Service |
| ASTM B515/ASME SB515 | Welded nickel-chromium-iron alloy tubes |
| ASTM B516, ASME SB516 | Welded nickel-chromium-iron alloy tubes |
| ASTM A554 | Specification for Welded Stainless Steel Mechanical Tubing |
| ASTM A632 | Standard Specification for Seamless and Welded Austenitic Stainless Steel Tubing (Small-Diameter) for General Service |
| ASTM A688/SA688 | Standard specification For Welded Austenitic Stainless Steel feedwater heater U Tubes |
| ASTM A731/A731M | Seamless and Welded Ferritic and Martensitic Stainless Steel Pipe |
| ASTM A778 | Specification for Welded, Unannealed Austenitic Stainless Steel Tubular Products |
| ASTM A789/A789M, ASME SA789/SA789M | Seamless and Welded Ferritic/Austenitic Stainless Steel Tubing for General Service |
| ASTM A790/A790M, ASME SA790/SA790M | Seamless and Welded Ferritic/Austenitic Stainless Steel Pipe |
| ASTM A450/A450M | Specification for General Requirements for Carbon, Ferritic Alloy, and Austenitic Alloy Steel Tubes |
| ASTM A530/A530M | Standard Specification for General Requirements for Specialized Carbon and Alloy Steel Pipe |
| ASTM A999/A999M | Specification for General Requirements for Alloy and Stainless Steel Pipe |
| ASTM A813/A813M | Standard Specification for Single- or Double-Welded Austenitic Stainless Steel Pipe |
| ASTM A814/A814M | Standard Specification for Cold-Worked Welded Austenitic Stainless Steel Pipe |
| ASTM A1016/A1016M | Standard Specification for General Requirements for Ferritic Alloy Steel, Austenitic Alloy Steel, and Stainless Steel Tubes |
| DIN 2463-1 | Welded austenitic stainless steel tubes: dimensions and masses per unit length |
| DIN 17455 | Welded circular stainless steel tubes with general quality requirements - Technical delivery conditions |
| DIN 17457 | Welded circular austenitic stainless steel tubes subject to special requirements |
| EN 10216-5 | Welded Stainless Steel Tube |
| EN 10217-7 | Welded steel tubes for pressure purposes - Technical delivery conditions - Part 7: Stainless steel tubes |
| EN 10296-2 | Welded circular steel tubes for mechanical and general engineering purposes - Technical delivery conditions - Part 2: Stainless steel |
| AS 1528 | Tubes (Stainless Steel) and Tube Fittings for the Food Industry |
| JIS G 3447 | Stainless Steel Sanitary Pipes |
| JIS G 3448 | Light Gauge Stainless Steel Tubes for Ordinary Piping |
| JIS G 3459 | Stainless Steel Pipes |
| JIS G 3468 | Large Diameter Welded Stainless Steel Pipes |
| JIS G 3463 | Stainless Steel Boiler and Heat Exchanger Tubes |
| JIS G 3446 | Stainless Steel Pipes for Machine and Structural Purposes |
Finned Tube Service Matching to Tube Standards
Buyers who come to us with a working condition rather than a standard number usually end up choosing from the groups below. It is a short cut, not a substitute for the datasheet.
| Duty | Standard family that fits | Why it fits |
|---|---|---|
| Condenser and heat exchanger tubes in austenitic stainless steel | ASTM A249/A249M | Written for welded boiler, superheater, heat exchanger and condenser tubes, with eddy current testing and a weld seam that accepts fin welding |
| Feedwater heater U tubes | ASTM A688/SA688 | Covers the U bend and the tighter inspection routine that a feedwater heater demands |
| Sanitary coils for dairy, beverage and pharmaceutical lines | ASTM A270, AS 1528, JIS G 3447 | Surface finish, weld dressing and cleanliness rules that survive clean in place cycles |
| Chloride bearing cooling water and marine air | ASTM A789/A789M, ASTM A790/A790M | Duplex and super duplex grades resist pitting and stress corrosion cracking |
| Structural frames and mechanical supports around the bundle | ASTM A554, JIS G 3446 | Mechanical tubing tolerances without the pressure service paperwork |
| High temperature flue gas and corrosive off gas | ASTM A358/A358M, ASTM A409/SA409 | Electric fusion welded large diameter pipe for high temperature and corrosive service |
Finned Tube Base Tube and Fin Pairing
How the fin meets the tube wall matters more than the fin shape on a catalogue page. The joining method sets the ceiling for working temperature, and the two metals have to be tolerant of each other through thousands of heating and cooling cycles.
| Pairing | How the joint is made | Fin material | Typical ceiling | Where it is used |
|---|---|---|---|---|
| Embedded fin, G fin | Fin foot is pressed into a groove rolled on the tube, then locked | Aluminium | Around 250 °C | Air cooled condensers, refrigeration evaporators |
| L, LL, KL wrapped fin | Fin is wound under tension and the foot is crimped or knurled onto the tube | Aluminium, copper | Around 150 to 200 °C | Air heaters, dryers, comfort coils |
| High frequency welded solid fin | Fin strip is resistance welded to the tube along a continuous spiral | Carbon steel, stainless steel, alloy steel | Above 400 °C | Boiler economisers, waste heat recovery |
| High frequency welded serrated fin | Same weld process, with the fin edge cut into segments | Carbon steel, stainless steel | Above 400 °C | Dusty or high viscosity flue gas streams |
| Laser welded fin | Laser beam fuses fin to tube with a narrow heat affected zone | Stainless steel, nickel alloy | High temperature duty | Compact exchangers, corrosive atmospheres |
| Expanded fin | Tube is expanded mechanically into the fin collar | Copper, aluminium | Moderate temperature | Copper tube aluminium fin air conditioning coils |
Finned Tube Cost and Lead Time Effects
Why does the same finned tube bundle come back with quotations that differ by thirty percent? The gap is normally in the base tube, not in the fin. A tube ordered to ASTM A249 with full eddy current testing, a controlled weld bead and a documented heat number costs more and takes longer than a tube bought to a general service grade, and the difference is real metal and real inspection hours.
Which standard you name also changes the mill route. Sanitary tubing to ASTM A270 needs a smoother internal and external finish, so it moves through additional polishing and passivation steps. Duplex tubing to ASTM A789 or A790 needs a controlled thermal cycle to keep the ferrite and austenite balance, which limits the number of mills that can supply it. Once you know the duty, matching it to the loosest acceptable standard is one of the few ways left to take cost out of a bundle without touching the thermal design.
Finned Tube Traceability and Documentation
For power, chemical and pharmaceutical projects, the paperwork travels with the tube. A mill test certificate tied to the heat number, an eddy current or hydrostatic test report, and a welding procedure record for the fin line are normally enough to close out an inspection release. Where the fin is welded to the tube, the heat input has to stay inside a range that does not degrade the tube wall, and that range should appear in the welding procedure rather than being left to the operator.
Corrosion allowance, minimum wall thickness and the acceptance level for the fin weld are the three items most often argued about at the inspection stage. Settling them at the quotation stage saves far more time than settling them after the bundle is built.
Finned Tube Questions from Engineers
What is the difference between a finned tube and a plain tube in a heat exchanger?
A plain tube transfers heat only through its outer surface, and the still boundary layer of air or flue gas slows that transfer down. A finned tube carries fins on the outer surface, which expands the area to 2 to 10 times that of a bare pipe and breaks the boundary layer into turbulence. The result is a higher heat transfer coefficient with less tube material.
Which tube standard applies to a stainless steel fin tube heat exchanger used in food processing?
Sanitary duty usually points to ASTM A270, AS 1528 or JIS G 3447, all of which control surface finish and weld quality closely. Where the coil is cleaned in place, the base tube should be ordered to one of these standards rather than to a general service grade.
How is the fin attached to the base tube?
It depends on the working temperature and the budget. Fins can be embedded into a groove rolled on the tube wall, wrapped and tensioned, welded by high frequency or laser, or expanded mechanically. Welded fins survive the highest tube wall temperatures, while embedded and wrapped fins are the cheapest option for refrigeration work.
Can the base tube and the fin be made of different metals?
Yes, and it is common practice. Aluminium fins on stainless or carbon steel base tubes are widely used, and copper fins on copper tubes appear in air conditioning coils. Because the two metals expand at different rates, the joining method has to be chosen so the fin does not loosen under thermal cycling.
How should a fin tube heat exchanger be specified?
Start from the heat load and the flow rates, then fix the base tube standard and size, the fin material, the fin pitch and the joining method. Naming the tube standard early keeps quotations comparable, because the standard decides wall thickness tolerance, non destructive testing level and lead time.