
Lord Fin Tube-Urea resistant stainless steel 00cr25ni22mo2n
Urea plants run some of the harshest chemistry found in any chemical works. Inside the synthesis loop, ammonium carbamate liquid sits at 180 °C to 200 °C under pressures reaching 200 bar, and ordinary stainless steels are eaten away within months. The heat exchange tubes and the plates that hold them both sit in that corrosion zone, which is why the two are normally ordered in the same grade — urea-grade 00cr25ni22mo2n.
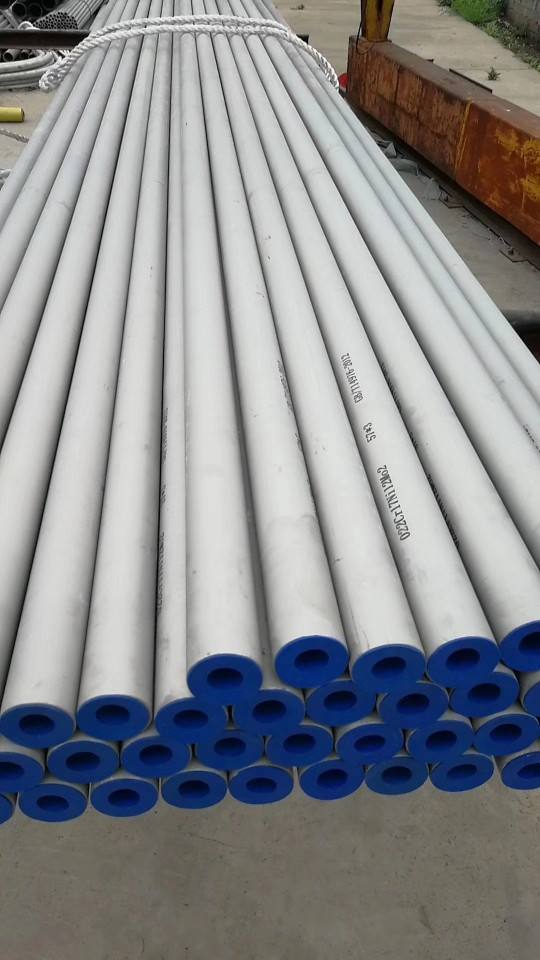
Urea resistant stainless steel 00cr25ni22mo2n
It is a low-carbon, high-chromium austenitic grade developed specifically for ammonium carbamate service. The designation itself tells most of the story: carbon held at or below 0.02 % (the "00" prefix), roughly 25 % chromium, 22 % nickel, 2 % to 3 % molybdenum, plus a deliberate nitrogen addition. This is not a tweaked 316L. Chromium, nickel and molybdenum are all pushed higher while carbon and silicon are pulled down, which suppresses both carbide precipitation and ferrite formation.
How the grade is named across standards
A single heat of this material travels under several names depending on which standard the mill certificate follows. Buyers comparing quotations from different suppliers often find the same alloy quoted under three or four designations.
| Naming system | Designation |
|---|---|
| Chinese GB | 00Cr25Ni22Mo2N |
| EN / DIN | 1.4466, X1CrNiMoN25-22-2 |
| UNS | S31050 |
| ASTM product specs | A312 TP310MoLN, A240 S31050 |
| Trade names in circulation | 725LN, 2RE69 |
What "urea grade" actually commits the mill to
Urea grade is not a separate alloy — it is a bundle of acceptance conditions layered on top of the chemistry. A heat that meets A240 or A312 chemistry alone is not automatically urea grade. The extra conditions cover ferrite content, a Huey corrosion test on the finished product, and in many cases a selective corrosion test run to the licensors own procedure. Two suppliers can both ship "S31050" and still deliver very different material depending on which of those conditions they actually tested.
Why urea plants specify urea resistant stainless steel 00cr25ni22mo2n
Ammonium carbamate does not attack metal the way seawater or dilute acid does. It goes after grain boundaries and any ferrite phase present, while simultaneously trying to strip the passive film off the surface. Chromium and molybdenum at these levels rebuild that film quickly; nitrogen strengthens it further. Nickel keeps the matrix fully austenitic so there is no second phase left for the medium to attack preferentially.
Three damage routes that decide service life
Wall thinning from general corrosion is the easiest to predict and usually the least dangerous. Grain boundary attack following chromium carbide or sigma precipitation is faster and harder to see. Selective attack, where ferrite stringers dissolve ahead of the surrounding austenite, produces pits that grow into through-wall leaks. The 00cr25ni22mo2n composition addresses all three: carbon under 0.02 % removes the driver for carbide precipitation, solution annealing restores a single-phase structure, and a Huey test on the finished tube or plate confirms the result.
Where the material is unavoidable
The stripper, the high-pressure carbamate condenser, urea reactor internals, and sections of the carbamate pump piping all see conditions where lower grades fail early. The tube-to-tubesheet joint deserves the closest attention, because that is where a weld, an expansion joint and a crevice sit within a few millimetres of each other.
Urea resistant stainless steel 00cr25ni22mo2n composition and properties
Ranges below follow the common product standards. Tighten or widen them only after checking which specification your project actually references, since licensor specifications sometimes narrow the windows further.
| Element | Content, % | What it does in service |
|---|---|---|
| C | ≤ 0.020 | Keeps carbon in solution so carbides cannot form at grain boundaries |
| Si | ≤ 0.70 | Restricted to limit ferrite and sigma phase |
| Mn | ≤ 2.00 | Austenite stabiliser, residual from deoxidation |
| P | ≤ 0.025 | Controlled for weldability and toughness |
| S | ≤ 0.010 | Low sulphur improves corrosion resistance and hot workability |
| Cr | 24.0 – 26.0 | Builds and repairs the passive film |
| Ni | 21.0 – 23.0 | Holds the structure fully austenitic |
| Mo | 2.00 – 3.00 | Resists carbamate attack and chloride pitting |
| N | 0.10 – 0.20 | Raises strength and stabilises the passive layer |
| Fe | Balance | — |
| Property | Typical requirement |
|---|---|
| 0.2 % proof stress, Rp0.2 | ≥ 250 MPa |
| Tensile strength, Rm | 540 – 690 MPa |
| Elongation, A | ≥ 40 % |
| Hardness | ≤ 95 HRB |
| Ferrite content | ≤ 0.6 % |
| Delivery condition | Solution annealed, pickled or bright annealed |
Urea resistant stainless steel 00cr25ni22mo2n compared with other grades
Substitution questions come up constantly during front-end engineering. The table below reflects how each grade behaves in a carbamate environment rather than how it performs in general corrosion testing.
| Grade | Cr % | Ni % | Mo % | Behaviour in urea synthesis |
|---|---|---|---|---|
| 316L | 16 – 18 | 10 – 14 | 2 – 3 | Corrodes too quickly in carbamate; not accepted for high-pressure loops |
| 904L / N08904 | 19 – 23 | 23 – 28 | 4 – 5 | Better than 316L but still limited; sometimes used in lower-pressure sections |
| 00Cr25Ni22Mo2n | 24 – 26 | 21 – 23 | 2 – 3 + N | Qualified urea grade; passes Huey testing after final heat treatment |
| Duplex 2205 | 22 | 5 | 3 | Unsuitable — the ferrite phase dissolves preferentially in carbamate |
Urea resistant stainless steel 00cr25ni22mo2n tube and tube sheet supply forms
The same heat can become either a seamless tube or a forged plate, but the manufacturing routes diverge early and the dimensional possibilities differ a great deal.
Tubes
Heat exchanger tubing is normally cold drawn and then solution annealed. Outside diameters of 19.05 mm, 25.4 mm, 31.75 mm and 38.1 mm cover most urea condenser and stripper designs, with wall thickness between 1.65 mm and 3.05 mm. Both straight lengths and U-bends can be supplied. Seamless 00Cr25Ni22Mo2N tube holds tighter wall tolerances and has no longitudinal weld seam, which matters where the tube passes through a thick tubesheet and is expanded on both sides.
Tube sheets
Plates are usually produced as forgings, upset from an ingot to near-net shape, then rough machined, solution annealed and ultrasonically inspected. Thickness commonly falls between 40 mm and 300 mm, with finished diameters reaching several metres on large condensers. The same grade is used for both components, and Urea resistant stainless steel 00cr25ni22mo2n tube sheet forgings are typically ordered to a licensor specification that adds ferrite and corrosion testing on top of the base standard.
| Item | Tube | Tube sheet |
|---|---|---|
| Production route | Cold drawn, solution annealed | Forged, solution annealed |
| Typical dimensions | OD 19.05 – 38.1 mm, WT 1.65 – 3.05 mm | Thickness 40 – 300 mm, OD up to several metres |
| Length or unit weight | Straight lengths or U-bends | Single pieces up to roughly 15 t |
| Surface condition | Pickled or bright annealed | Rough machined or finish machined |
| Core non-destructive tests | Eddy current, hydrostatic, ultrasonic | Ultrasonic, dye penetrant, hardness survey |
Urea resistant stainless steel 00cr25ni22mo2n corrosion verification
Chemistry alone proves very little. What decides whether a batch is accepted into a urea plant is the test package that accompanies it.
The Huey test
Run to ASTM A262 Practice C in boiling 65 % nitric acid. The sample passes through several 48-hour cycles and the corrosion rate for each cycle must stay below the agreed ceiling — usually in the region of 3.3 µm per cycle for urea-grade material. The test is designed to expose grain boundary attack, which is exactly the failure mode that sensitised material shows first.
Ferrite content
Measured metallographically or magnetically. Urea specifications normally cap ferrite at 0.6 %, and some licensors tighten that further. The reason is straightforward: in ammonium carbamate, ferrite dissolves ahead of austenite, creating pits that eventually become leak paths through the tubesheet ligament.
Selective and intergranular corrosion tests
Project specifications sometimes call for a selective corrosion test run to a licensor procedure, in addition to Practice B or Practice E of ASTM A262. These are not always applied on every heat, but the tender documents usually state whether they are mandatory or only required on a sampling basis.
Urea resistant stainless steel 00cr25ni22mo2n machining and fabrication
This grade work hardens quickly. A drill or insert that dwells in one spot raises surface hardness, and the cutting edge starts to wear against the hardened layer instead of cutting cleanly. The whole machining sequence has to be arranged around that behaviour.
Tubesheet drilling
Low spindle speeds, constant feed and generous coolant volume. Chloride-bearing cutting fluids must be avoided — the grade resists chlorides far better than 304 or 316, but contaminated water-based coolant still creates a pitting risk that shows up later as a failed penetrant test. Peck drilling cycles help control heat on deep holes, and gun drilling is used where hole depth exceeds roughly five times the diameter.
Tube end preparation and expansion
Tube ends are cut to length, deburred, and finished to a surface roughness that matches the chosen joining method. Hydraulic expansion produces uniform contact along the hole, and a seal weld at the tube end provides the final barrier. Clearance between hole and tube outside diameter has to be held tightly, because excessive clearance reduces the pull-out strength of the expanded joint.
Urea resistant stainless steel 00cr25ni22mo2n welding
Filler metal chemistry should match the base metal closely — around 25 % Cr, 22 % Ni, 2 % Mo with nitrogen, supplied as bare wire for TIG. Heat input and interpass temperature must both be controlled, because an overheated heat-affected zone can precipitate secondary phases and fail the Huey test even when the chemistry is correct.
Tube-to-tubesheet joints
Automatic TIG welding is standard, with deep penetration or bore welding used on thicker plates depending on the joint design. Every pass is cleaned before the next one starts, and shielding gas coverage on the back side must be verified — an oxidised root loses corrosion resistance that cannot be restored by pickling alone.
Qualification and inspection of welds
Procedure qualification to ASME IX, visual and non-destructive examination, and where the owner requires it, a Huey test on a welded coupon. For critical equipment, some projects specify witnessed testing under EN 10204 3.2 rather than a simple mill certificate.
Urea resistant stainless steel 00cr25ni22mo2n purchasing checks
Unit prices for this grade vary widely, and the gap is rarely explained by nickel alone. It usually comes down to how much testing the mill actually performed. The list below is worth working through before a purchase order is released.
| Item to verify | Why it matters |
|---|---|
| Heat traceability | Tube and tubesheet are often required from matched or separately certified heats |
| Heat treatment record | Solution annealing temperature and hold time determine corrosion performance |
| Huey test report | Demonstrates intergranular corrosion resistance on the finished product |
| Ferrite measurement | Confirms the structure is essentially fully austenitic |
| Non-destructive test reports | Ultrasonic for plates, eddy current or hydrostatic for tubes |
| Certificate type | EN 10204 3.1 as a minimum, 3.2 for safety-critical equipment |
| Third-party inspection | TÜV, BV, SGS or an owner-nominated inspector witnessing the tests |
Lead times follow the production route rather than the grade. Cold drawn tubing typically runs six to ten weeks from a confirmed order, while large forged tubesheets often need twelve to sixteen weeks because the forging, heat treatment and ultrasonic inspection steps cannot be compressed. Ordering tube and plate together from the same supplier usually shortens the overall schedule, since heat matching can be planned at the melting stage rather than resolved afterwards.
Urea resistant stainless steel 00cr25ni22mo2n questions buyers ask
Is 00Cr25Ni22Mo2N the same as 725LN?
In practical terms, yes. The two names describe the same alloy family with the same chemistry window. What differs is the specification the material is certified against, and that is what determines the test package you receive.
Why is ferrite capped at 0.6 %?
Because ferrite is the phase that carbamate attacks first. A tube or tubesheet with higher ferrite may pass a tensile test and still develop pits within a short time in service, particularly along the ligament between adjacent holes.
Can 00Cr25Ni22Mo2n be used where 316L was originally specified?
It is a direct upgrade in corrosion terms, but the substitution still has to be reviewed for weld procedure qualification, expansion force settings and thermal expansion differences. Upgrading without re-qualifying the fabrication procedures creates a different set of problems.
Which tube sizes are normally stocked or readily produced?
Outside diameters of 19.05 mm, 25.4 mm and 31.75 mm with 1.65 mm to 2.77 mm walls are the most common. Non-standard sizes are possible but extend the lead time because new drawing dies are usually required.
How long does a Huey test take?
Each cycle runs 48 hours and most specifications require at least five cycles, so the test alone consumes roughly ten days. That period needs to be built into the delivery schedule rather than treated as an afterthought.