
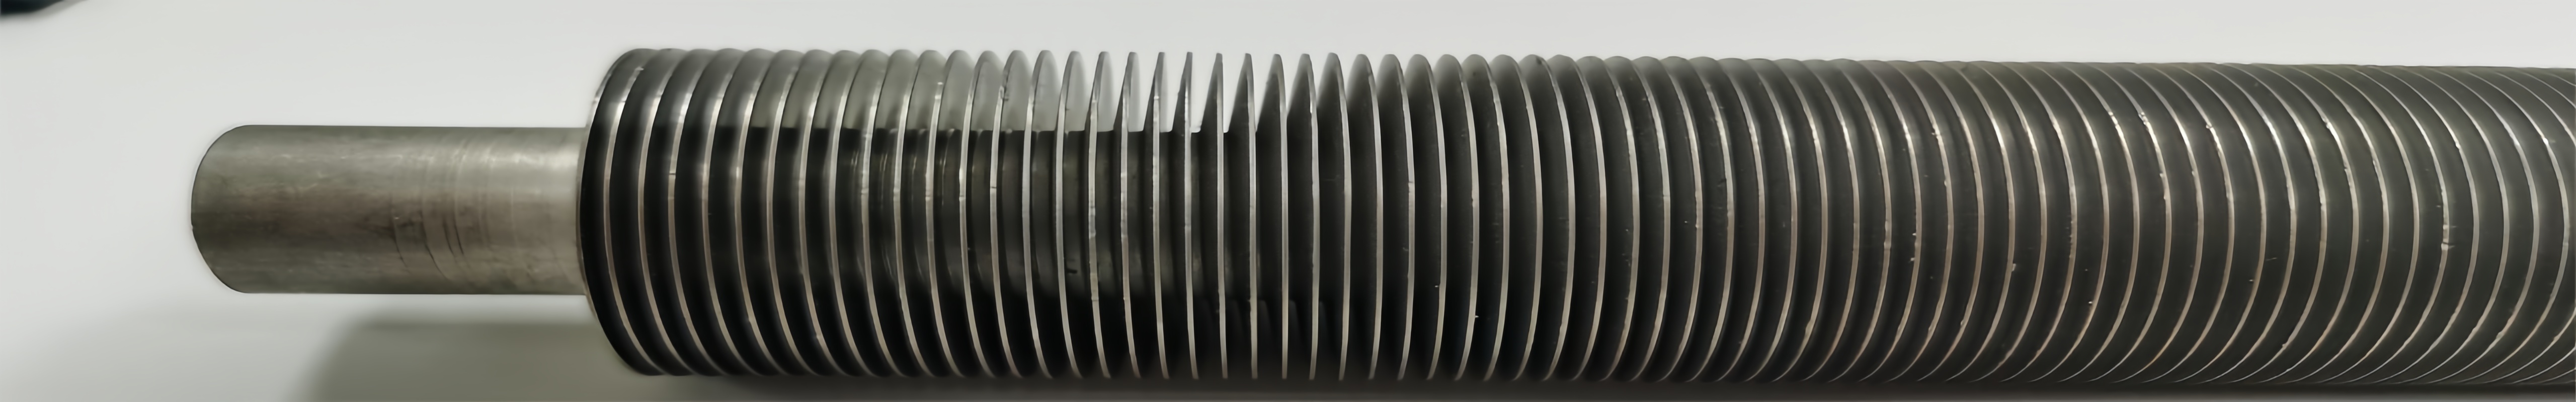
Refinery air coolers, also known as air cooled heat exchangers (ACHE), are critical heat rejection equipment used across crude distillation, hydrocracking, reforming and overhead condensation circuits. Aluminum finned tubes serve as the core heat transfer component inside these units, where they transfer process heat from the internal tube fluid to ambient air forced across the external fin surface. Among multiple fin manufacturing technologies, extruded fin tube remains the preferred selection for refinery overhead condenser finned tube applications due to robust mechanical bonding, high thermal conductivity and resistance to thermal cycling.
What are Aluminum Finned Tubes for Refinery Air Coolers?
Aluminum finned tubes consist of a base tube, which carries the hot refinery process medium, and external aluminum fins engineered to expand the heat exchange area. In refinery air coolers, process fluid flows inside the base tube while cooling air flows crosswise over the aluminum fins. The large extended fin surface drastically increases convective heat transfer with air, which has inherently low heat transfer coefficients compared with liquid cooling media.
Extruded fin tube construction forms fins from a solid aluminum sleeve extruded under high pressure onto the outer surface of the base tube. This process creates a metallurgically tight contact between fin and base tube, eliminating air gaps that degrade thermal performance. This design distinguishes extruded aluminum finned tubes from wrapped or L-foot fin types, especially under the frequent temperature fluctuations common in refinery overhead condenser finned tube service.
Key Definition: Air Cooled Heat Exchanger (ACHE) in Refinery Service
An air cooled heat exchanger uses atmospheric air as the cooling medium instead of cooling water. Refineries deploy ACHEs where water resources are limited, or where process safety rules reduce the risk of water-side fouling and leakage mixing with hydrocarbon streams. Each ACHE bundle is assembled from hundreds of finned tubes arranged in parallel rows, mounted within a frame and paired with large axial fans. The aluminum finned tubes are the primary heat transfer hardware for this system.
Refinery overhead condenser finned tube is a specialized subset of aluminum finned tubes. It is installed in overhead condenser ACHEs, which cool and condense hot vapor streams from the top of crude distillation columns. This service imposes specific demands: cyclic temperature changes, occasional corrosive vapor traces and vibration from fan operation, making fin bond integrity a critical design requirement.
Critical Parameters and Units for Aluminum Finned Tubes
1. Fin Density
Fin density describes the number of fins per unit length along the tube axis, usually expressed as fins per inch (FPI). Typical range: 7 to 11 FPI for refinery ACHE service. Final selection to be confirmed by project thermal rating and engineer specification. Higher fin density increases total heat transfer area, but also raises air-side pressure drop and fouling tendency.
2. Fin Height
Fin height is the radial distance from the base tube outer wall to the fin tip, measured in mm or inches. Typical range: 12.5 mm to 16 mm. Taller fins add surface area, but fin efficiency decreases as height increases, because heat must travel farther through aluminum to reach the fin tip.
3. Fin Thickness
Fin thickness refers to the material thickness of the aluminum fin web, usually in mm. Typical range: 0.35 mm to 0.5 mm. Thicker fins improve mechanical rigidity and reduce vibration fatigue risk, at the cost of slightly higher material weight and reduced fin count for fixed raw aluminum volume.
4. Base Tube Outer Diameter
Base tube OD is the outside diameter of the inner process tube, measured in mm or inches. Typical range: 25 mm to 50 mm for refinery air cooler bundles. Base tube material is selected separately for process fluid corrosion and pressure containment, while aluminum provides the extended fin surface.
Formula and Calculation
Not applicable to this product type for simplified article scope. Complete ACHE thermal rating requires professional heat exchanger simulation software. Key calculation concepts used by thermal engineers are summarized below:
- Total heat duty Q = U × A × ΔTlm, where U = overall heat transfer coefficient, A = total heat transfer area, ΔTlm = log mean temperature difference.
- Fin efficiency ηf: ratio of actual heat transferred by a fin to the heat transfer if the whole fin were at base tube wall temperature. Fin efficiency falls with taller fins, thinner fins and higher air-side heat transfer coefficients.
- Air-side pressure drop: function of fin pitch, fin height, tube row count, air face velocity and fin surface fouling resistance.
All calculations must be validated by the heat exchanger vendor and process engineer, and final dimensions shall follow project specification.
Comparison Table: Extruded Aluminum Finned Tubes vs Other Fin Types for Refinery ACHE
| Fin Tube Type | Fin Bond Strength | Thermal Contact Resistance | Resistance to Thermal Cycling | Typical Refinery Suitability |
|---|---|---|---|---|
| Extruded fin tube | Excellent, solid mechanical interlock | Very low | High, minimal risk of fin loosening | Preferred for overhead condenser and cyclic service |
| L-foot wrapped fin tube | Good, dependent on wrapping tension | Moderate | Moderate, may loosen under repeated thermal expansion | Suitable for steady temperature non-critical circuits |
| Embedded/G-type fin tube | Good, fin root locked into tube groove | Low | Good | Used for high temperature, but higher manufacturing cost |
| Spot welded fin | Limited at discrete weld points | Higher contact resistance | Poor under cyclic heating | Not recommended for refinery overhead condenser service |
Design and Selection Tradeoffs
Designing aluminum finned tubes for refinery air coolers requires balancing thermal performance, pressure drop, fouling risk, mechanical durability and capital cost. These tradeoffs must be reviewed by the heat transfer engineer before final bundle specification.
- Fin density tradeoff: Higher FPI increases heat transfer area, which can reduce the required bundle size. However, dense fins trap dust, hydrocarbon particulates and airborne debris, increasing fouling and air-side pressure drop. Higher fan power consumption and more frequent cleaning become necessary.
- Fin height tradeoff: Increasing fin height adds surface area, but fin efficiency drops. Beyond a certain height, extra aluminum material delivers little additional heat transfer and increases tube bundle weight.
- Material tradeoff: Aluminum fins offer low cost, low density and high thermal conductivity. Aluminum is not suitable if the local environment contains heavy chloride deposition or high temperature corrosive gases; alternative fin materials shall be evaluated for such cases.
- Bundle arrangement tradeoff: More tube rows improve heat recovery but increase air pressure drop and fan energy use. Refinery ACHE design balances the number of tube rows against operating power cost over the equipment lifecycle.
Technical Parameter Table (Typical Range)
| Parameter | Typical Range | Remarks |
|---|---|---|
| Fin Material | Aluminum 1060 / 1050 | High thermal conductivity; to be confirmed by project specification |
| Base Tube Material | Carbon steel, stainless steel, alloy steel | Selected for process pressure, corrosion and temperature |
| Fin Density | 7–11 FPI | Common for refinery ACHE bundles |
| Fin Height | 12.5–16 mm | Typical range; final by thermal design |
| Fin Thickness | 0.35–0.5 mm | Balances rigidity and heat transfer performance |
| Base Tube OD | 25–50 mm | Common ACHE tube sizes |
| Length | Up to 12 m | Custom cut per bundle drawing |
| Applicable Standards | according to project specification | to be confirmed |
Materials and Applicable Standards
Aluminum alloy 1060 or 1050 is the standard fin material for extruded fin tube for refinery ACHE, chosen for excellent thermal conductivity, formability and reasonable cost. The base tube is a separate pressure-containing component. Base tube material selection depends entirely on the process fluid inside the tube: carbon steel for non-corrosive hydrocarbon streams, stainless steel or alloy steel for sour service, high temperature or corrosive overhead vapor.
All manufacturing, dimensional inspection and material acceptance follow applicable project specification, to be confirmed before order release. Material test certificates and dimensional reports can be supplied per buyer requirements.
Application Industries and Refinery Service Scenarios
Primary application industry: petroleum refining. Within refineries, aluminum finned tubes for air cooler are deployed in these typical circuits:
- Crude unit overhead condensers (refinery overhead condenser finned tube)
- Hydrotreating and hydrocracking product coolers
- Reformer recycle gas cooling
- Vacuum unit overhead air cooled heat exchangers
- Compressor interstage and aftercoolers
- Process water and utility hydrocarbon cooling loops
Refineries prefer air cooled heat exchangers in regions where cooling water is scarce, expensive or subject to strict environmental discharge limits. Aluminum finned tube bundles avoid many water cooling system problems such as cooling tower blowdown, water-side scaling and circulating pump maintenance.
Selection Guide for Aluminum Finned Tubes in Refinery ACHE
Follow these key selection steps when specifying extruded fin tube for refinery ACHE:
- Define process heat duty, inlet and outlet temperatures, design pressure and fluid composition of the stream inside the base tube.
- Identify ambient design air temperature, site altitude, wind conditions and expected airborne fouling load.
- Select base tube material compatible with process fluid corrosion, hydrogen attack or sulfide stress cracking risks.
- Select fin material, fin density, fin height and fin thickness to meet thermal performance while controlling air-side pressure drop and fouling potential.
- Confirm fin manufacturing method: extruded fin tube is strongly recommended for overhead condenser circuits with thermal cycling.
- Verify bundle arrangement, tube length, header connection type and mechanical vibration checks for fan-induced vibration.
- Agree inspection scope, material certificates and dimensional tolerance requirements before production.
Quality Control and Testing Items
Typical quality tests for aluminum finned tubes for refinery air cooler, final test scope subject to project specification:
- Raw material PMI and material certificate verification for base tube and aluminum fin sleeve
- Dimensional inspection: base tube OD, wall thickness, fin height, fin density, fin thickness, straightness and length
- Fin bond tightness check for extruded fin tube to confirm no loose fins
- Visual inspection for surface scratches, cracks, deformation and extrusion defects
- Hydrostatic test or air pressure test of base tube as required by project
- Sampling check for fin pull-out resistance when specified by buyer
Packing and Shipping Requirements
Typical packing and shipping for long finned tube bundles. Final packing scheme to be confirmed by order and logistics requirements:
- Finned tubes are bundled with protective separators to prevent fin crushing during transport.
- Tube ends are capped to avoid debris entering the base tube bore.
- Waterproof wrapping and wooden crate or steel frame packing for ocean or overland shipment.
- Identification tags with part number, heat number, quantity and project mark attached to each bundle.
- Stacking limits are marked to prevent excessive weight damaging the delicate aluminum fins.
- Loading plan designed to avoid point contact and vibration damage during transit.
Frequently Asked Questions
Aluminum has much higher thermal conductivity than carbon steel, which delivers far better heat transfer performance on the air side. Aluminum is lightweight and can be extruded into thin, high-efficiency fins. Steel fins are heavier and usually reserved for extreme high-temperature environments where aluminum cannot survive.
Refinery overhead condenser finned tube is an aluminum finned tube installed in ACHE overhead condensers on crude distillation columns. It cools and condenses hot overhead vapor. This service involves thermal cycling and vibration, so extruded fin tube construction is preferred for reliable fin bonding.
Extruded fin tube forms a solid interlocked fin root with minimal thermal contact resistance. It resists loosening under repeated thermal expansion and contraction, which is the main failure mode of wrapped L-foot fins in cyclic refinery service.
Higher fin density increases heat transfer surface area, reducing bundle footprint. The downside is higher air pressure drop, increased fan power consumption and higher fouling tendency. Refinery sites with dusty or oily atmospheres usually select lower fin density for easier cleaning.
Yes. Low-pressure air blowing or low-pressure water washing is commonly used to remove dust and oily deposits. High-pressure jet cleaning must be carefully controlled to avoid bending or tearing aluminum fins. Cleaning frequency depends on site environment and process leakage risk.
Extruded aluminum sleeves can be applied over carbon steel, stainless steel and alloy steel base tubes. The base tube material is selected separately for process pressure and corrosion resistance. The aluminum fin only provides the external heat transfer surface.
Typical maximum length can reach up to 12 m. Actual length is limited by heat exchanger bundle design, manufacturing capacity and transport constraints. All tube lengths are custom fabricated according to the ACHE drawing.
Request a Quote for Aluminum Finned Tubes for Refinery Air Cooler
Lordfintube supplies aluminum finned tubes and extruded fin tube for refinery air cooled heat exchangers and overhead condenser projects. Send your thermal datasheet, bundle drawing and specification to our engineering team for technical review and quotation.
Request a Quote