
Shell-and-Tube Heat Exchangers for Pulp & Paper
Shell-and-Tube Heat Exchangers for Pulp & Paper
Shell-and-tube heat exchangers are essential thermal equipment in pulp and paper manufacturing. They widely serve digesters, recovery boilers, bleaching lines and paper machine drying sections. These industrial heat exchangers withstand harsh process media, including black liquor, white liquor, green liquor, pulp stock and corrosive chemical solutions. Proper selection, operation and maintenance directly improve pulp mill energy efficiency, production uptime and paper product quality.
This article introduces the working principles, design advantages, common fouling problems, material selection standards and maintenance strategies of shell-and-tube heat exchangers for pulp and paper applications. It provides practical technical guidance for mill engineers and procurement teams.
What makes Shell-and-Tube Heat Exchangers for Pulp & Paper the go‑to solution for mill thermal systems? Their rugged construction, field‑proven reliability and adaptability to corrosive, fiber‑laden fluids give them a clear edge over other exchanger types in continuous pulp production environments.
Shell-and-Tube Heat Exchangers for Pulp & Paper: Industrial Advantages
Pulp and paper process fluids contain suspended fibers, abrasive particles and complex corrosive components with large temperature variations. Shell-and-tube heat exchangers are the most reliable solution for mill thermal systems due to the following strengths:
- Rugged structure resists fibrous liquids, high-solid media and abrasive flow conditions
- Detachable tube bundles allow easy cleaning and routine maintenance
- Multiple material options cover clean water, high-temperature flue gas and strong corrosive environments
- Flexible horizontal or vertical layout adapts to different process pipe arrangements
- High-temperature tolerance supports recovery boiler economizer operation at 180–300°C
Common Applications
Black liquor cooling and heating, white water cooling, pulp stock heating, chemical dosing cooling, vacuum pump seal water cooling, hydraulic oil cooling and bleaching tower temperature control.
Key Design Features
Pulp and paper heat exchangers adopt large flow areas, enhanced heat transfer tubes, removable heads, anti-corrosion structures and complete venting and drainage systems to avoid blockage, water hammer and stagnant corrosion.
Shell-and-Tube Heat Exchangers for Pulp & Paper: Fouling and Loss Analysis
Fouling is the most common failure cause for pulp mill heat exchangers. Inorganic scales such as calcium carbonate and calcium sulfate easily form on hot tube surfaces. Wood fibers, colloids, silica, phosphate, iron oxide, organic tar and biofilms further accumulate and block heat transfer surfaces.
Scaling sharply reduces thermal efficiency. Industrial data shows heat exchanger fouling causes huge energy waste and maintenance costs. Most operating units lose 15%–40% heat transfer performance before scheduled cleaning. White water with high suspended solids leads to hard scaling and under-deposit corrosion, greatly shortening equipment service life.
Common Foulants and Solutions
| Foulant | Source | Treatment |
|---|---|---|
| Calcium Carbonate | Cooling water, white water loops | Acid cleaning, phosphonate inhibitors |
| Calcium Sulfate | High-hardness water, evaporator systems | EDTA cleaning, temperature control |
| Wood Fibers & Colloids | Pulp stock, process streams | Large-diameter tubes, straight-through design |
| Silica & Aluminosilicate | Kraft liquor systems | Special antiscalants, water chemistry adjustment |
Which cleaning method works best for each foulant? Acid cleaning effectively removes carbonate scales, while EDTA chelation is preferred for sulfate deposits. Mechanical cleaning with rotating tube brushes handles fibrous and organic accumulations without chemical hazards.
Shell-and-Tube Heat Exchangers for Pulp & Paper: Recovery Boiler Integration
Recovery boilers generate large amounts of 180–300°C flue gas with reusable waste heat. Economizers and Heat Recovery Steam Generators preheat boiler feedwater and process water, effectively reducing steam consumption and fuel costs.
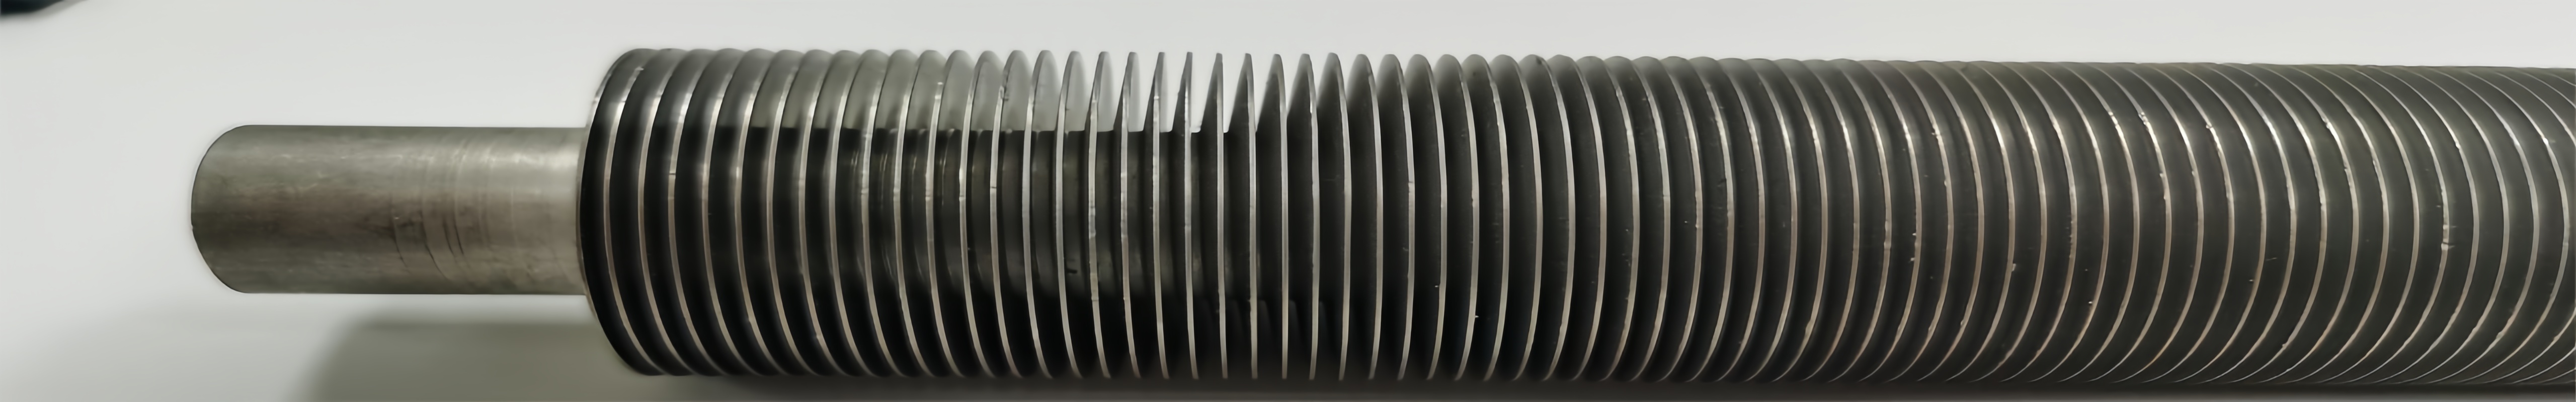
Different economizer types fit different working conditions. Cast Iron Economizer units offer stable corrosion resistance. H-Fin Tube Economizer designs provide large heat transfer area with low gas pressure drop. Studded Pipe Economizer configurations resist particle abrasion for high-dust flue gas.
304L stainless steel is the mainstream material for recovery boiler economizers to resist acidic condensate and particle erosion. Multi-stage installation achieves higher waste heat recovery efficiency.
| Economizer Type | Best Application | Key Benefit |
|---|---|---|
| Cast Iron Gilled Tube | Medium-corrosion flue gas | Corrosion resistance, stable operation |
| H-Fin Tube | Clean gas streams | Large heat transfer area, low pressure drop |
| Studded Pipe | High-dust, abrasive flue gas | Erosion resistance, durable fins |
Shell-and-Tube Heat Exchangers for Pulp & Paper: Material Selection
Material selection determines equipment service life under complex mill working conditions. Improper materials easily cause corrosion, cracking and erosion failure.
| Material | Application | Limitation / Note |
|---|---|---|
| Carbon Steel | Clean water, general utility pipelines | Not suitable for acid, chloride or caustic media |
| SS 304L | Recovery boiler flue gas, medium-corrosion environments | Good general resistance |
| SS 316L | White liquor, green liquor, bleaching chemicals | Higher chloride resistance than 304L |
| Duplex Steel | High-chloride, high-temperature process conditions | Requires careful welding procedure |
| Titanium | Severe corrosive bleach, chlorine dioxide media | Very high cost, reserved for extreme duties |
| Hastelloy C276 | Extreme reducing, pitting corrosion environments | Premium material for most demanding services |
Different metal combinations may cause galvanic corrosion. Matching compatible materials and applying tube sheet cladding effectively avoid accelerated corrosion failure. How do you select the right alloy for your specific liquor stream? Start with a thorough analysis of pH, chloride content, temperature and presence of oxidizing agents.
Shell-and-Tube Heat Exchangers for Pulp & Paper: Design Standards
To adapt to fiber-containing, easy-scaling and corrosive media, pulp and paper heat exchangers require targeted design optimization:
What design features most effectively combat fiber fouling? Large‑diameter tubes, generous nozzle sizes and straight‑through flow paths minimize blockages. Removable channel covers and full‑diameter tube bundles simplify mechanical cleaning during mill shutdowns.
Shell-and-Tube Heat Exchangers for Pulp & Paper: Maintenance Strategies
Preventive scale control is more efficient than post-fouling cleaning. Online protection includes scale inhibitors, dispersants and stable water chemical treatment. Offline maintenance includes acid cleaning, EDTA cleaning and mechanical tube cleaning.
Special antiscalants effectively reduce calcium oxalate scaling in evaporator systems. Physical water treatment devices also soften hard scale for easy flushing removal.
| Maintenance Method | Application | Typical Frequency |
|---|---|---|
| Acid cleaning (HCl / H2SO4) | Carbonate and oxide scales | Every 6–12 months |
| EDTA chelation cleaning | Sulfate and complex scales | As needed (based on U‑value drop) |
| Mechanical tube brushing | Fibrous and organic deposits | During scheduled shutdowns |
| High‑pressure water jetting | Stubborn fouling layers | Annual or semi‑annual |
Why is online chemical treatment preferred over offline cleaning? Continuous inhibitor dosing prevents scale nucleation and maintains heat transfer efficiency over longer periods, reducing production interruptions and extending tube bundle life.
Shell-and-Tube Heat Exchangers for Pulp & Paper: Performance Monitoring
Mill teams can judge heat exchanger operating status through key parameters:
| Indicator | Action Threshold |
|---|---|
| Heat transfer coefficient (U‑value) | Arrange cleaning when efficiency drops 15%–20% |
| Shell side & tube side pressure drop | Inspect abnormal flow resistance increases |
| Approach temperature | Monitor heat transfer uniformity |
| Outlet temperature stability | Ensure process production stability |
How often should performance indicators be reviewed? Daily logging of inlet/outlet temperatures and flow rates allows early detection of fouling trends. Weekly U‑value calculations provide a reliable basis for scheduling maintenance actions.
Shell-and-Tube Heat Exchangers for Pulp & Paper: Operational Reliability
Shell-and-tube heat exchangers are indispensable thermal equipment in modern pulp and paper factories. Reasonable material selection, anti-fouling structural design, regular performance monitoring and scientific maintenance can significantly improve energy saving effects, reduce operating costs and achieve long-term stable operation.
Which operational practices deliver the greatest reliability gains? Implementing a predictive maintenance program based on real‑time U‑value tracking, combined with periodic tube bundle inspections, has proven to extend exchanger service life by 30% or more in kraft mills.